
Blade Application Guides
Browse focused application knowledge
Cutting guides by industry, process, equipment and defect
Use these curated topic pages to compare related materials and cutting conditions without relying on broad site search.
Industries
Cutting processes
Equipment types
Cutting defects
Technical Articles
Industrial cutting problem knowledge base
1857 Blade Application Guides
Search by material, industry, cutting process or a problem described in your own words. You do not need to know the exact blade name.
Rubber, Tires & Gaskets
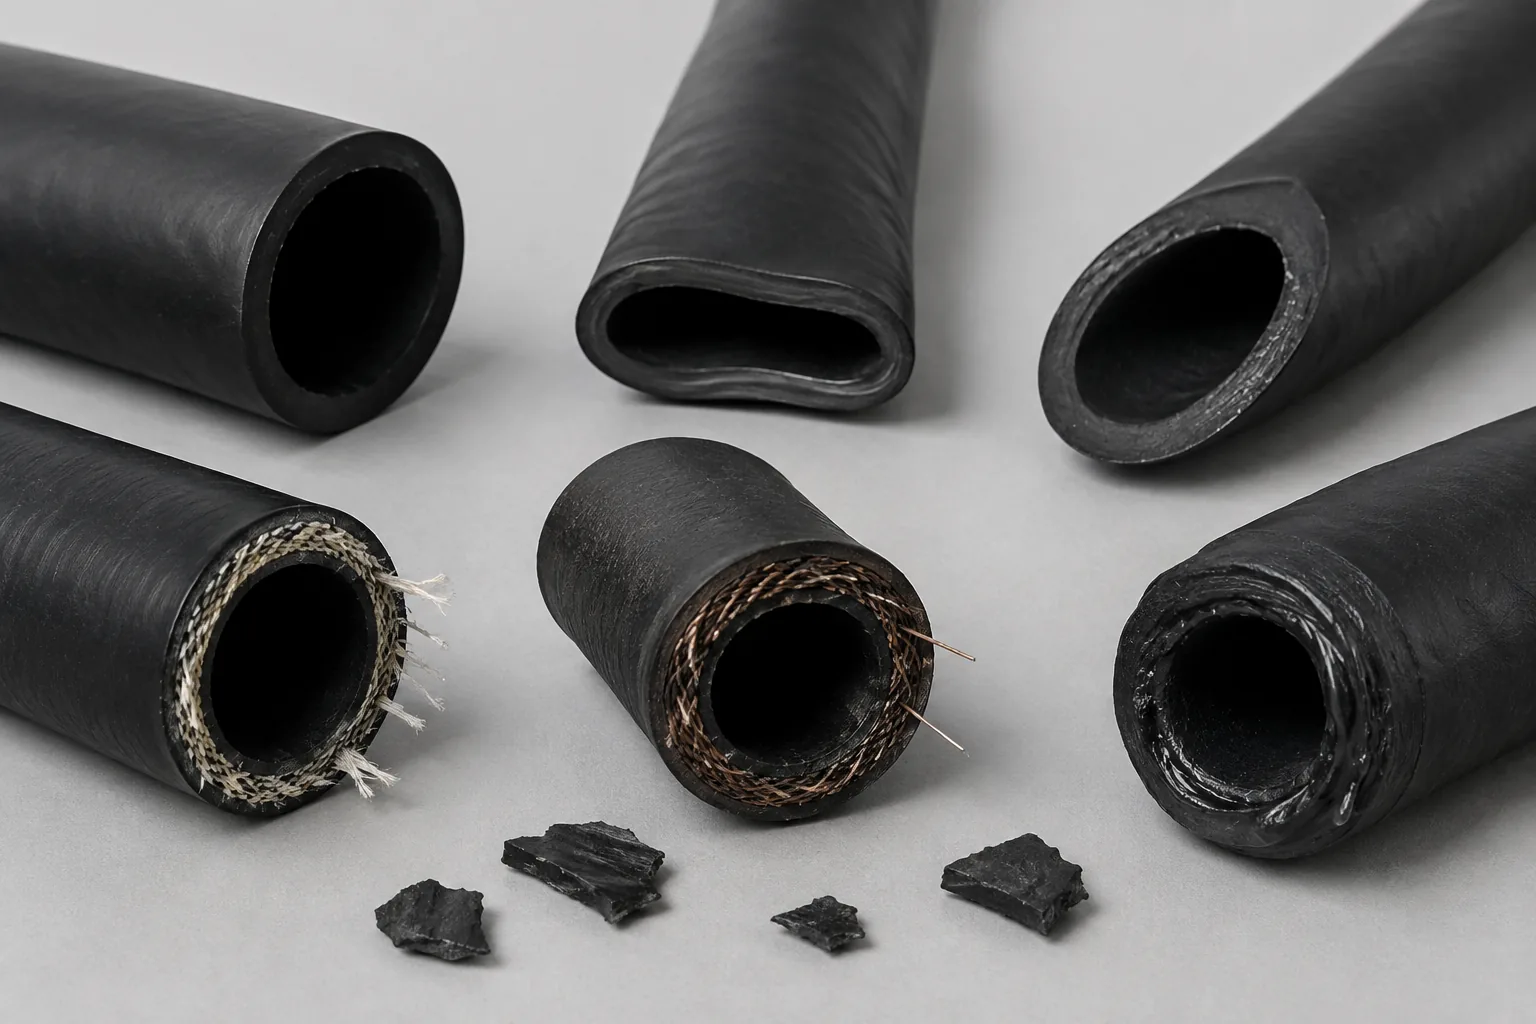
Rubber Hose Cutoff for Square Uncollapsed Ends
Review rubber hose cutoff for square ends, an open bore, clean reinforcement, controlled length, low rubber smear, and efficient chip removal.
Read the application guide →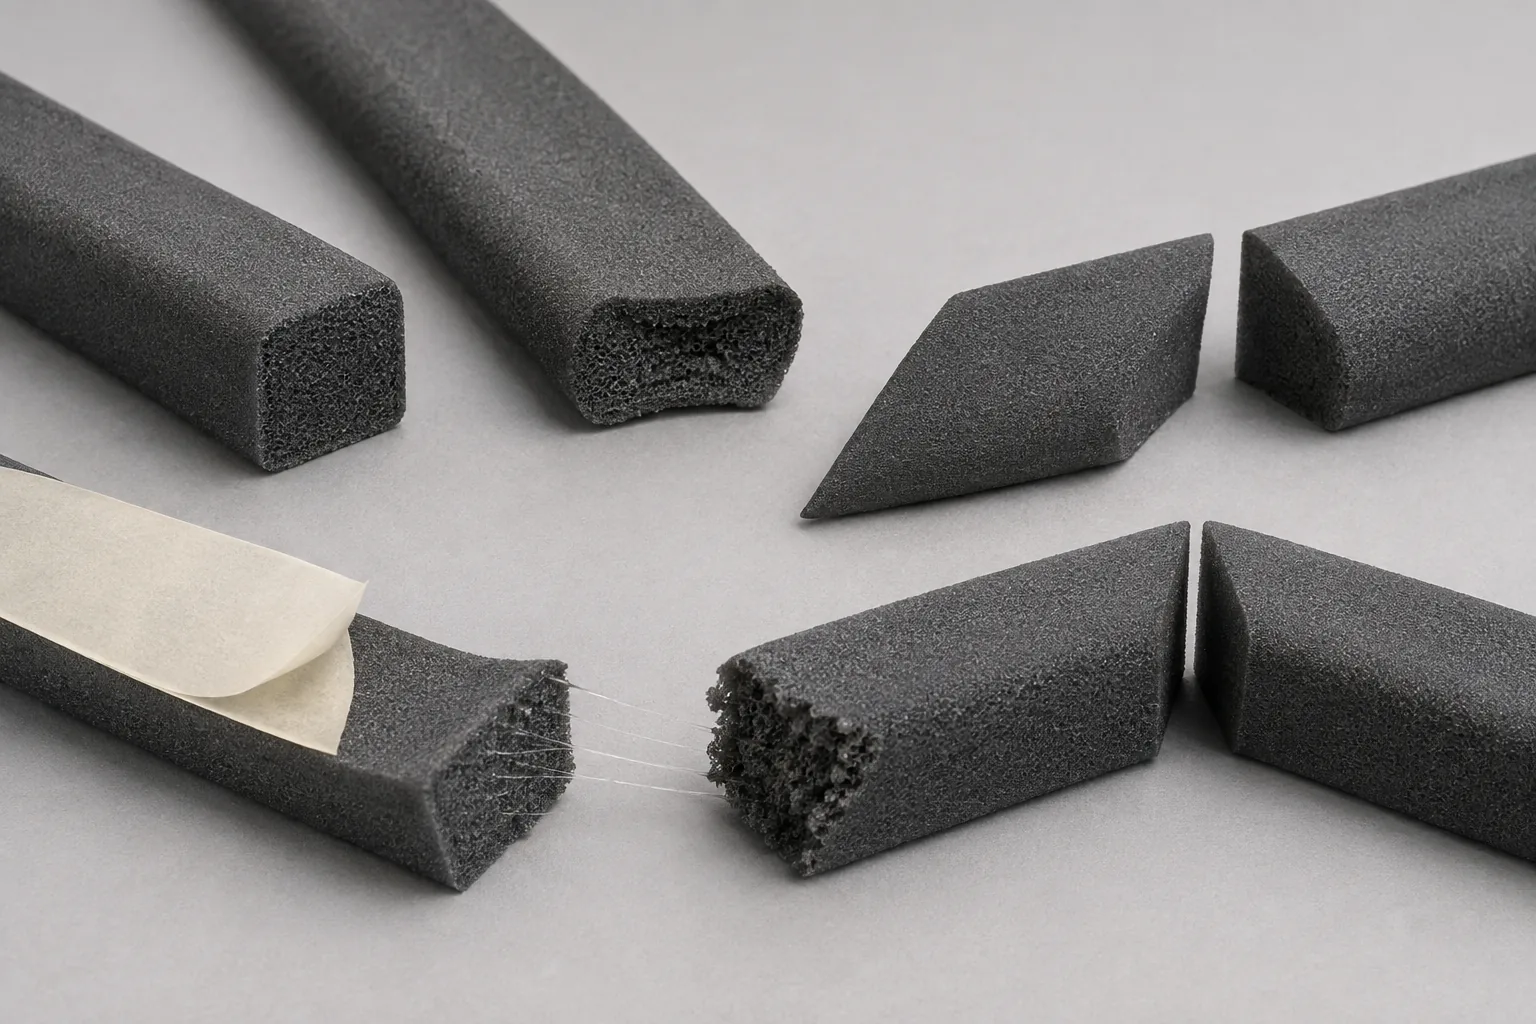
Rubber, Tires & Gaskets
Foam Sealing Strip Cutting Without Compression Set
Review foam sealing strip cutting for recovered length, square or mitered ends, intact cells, clean adhesive liners, and repeatable joint fit.
Read the application guide →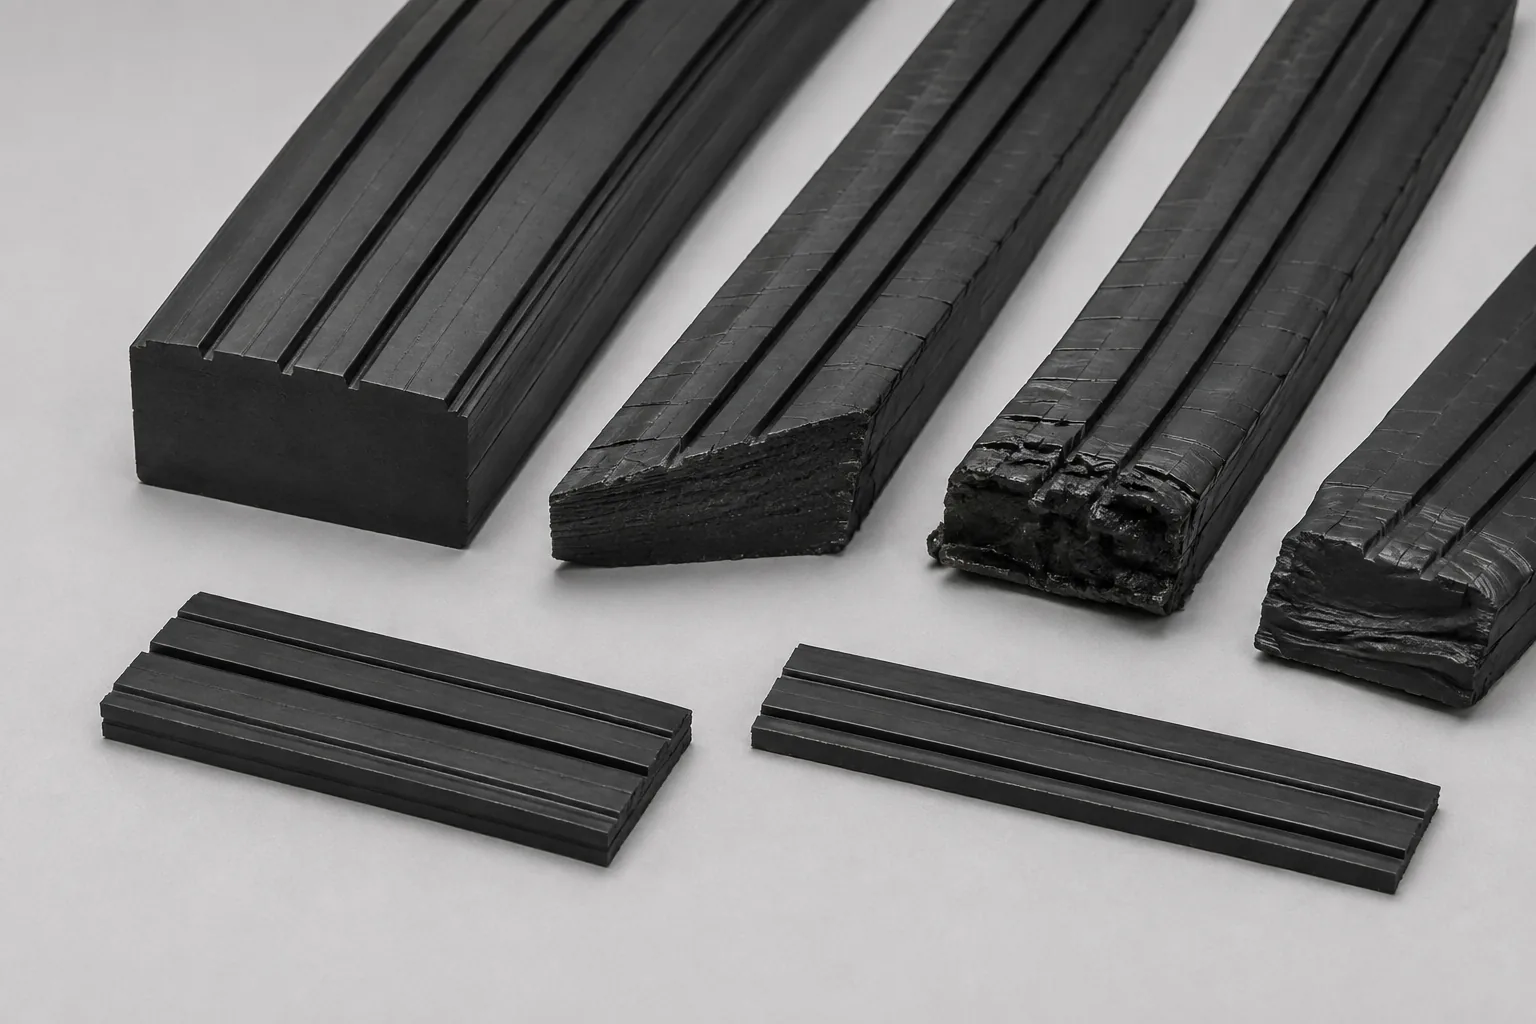
Rubber, Tires & Gaskets
Cutting Uncured Tire Tread Rubber Strips
Technical guidance for cross-cutting tacky, uncured tire tread: control cut length and face angle while limiting drag, deformation and rubber buildup.
Read the application guide →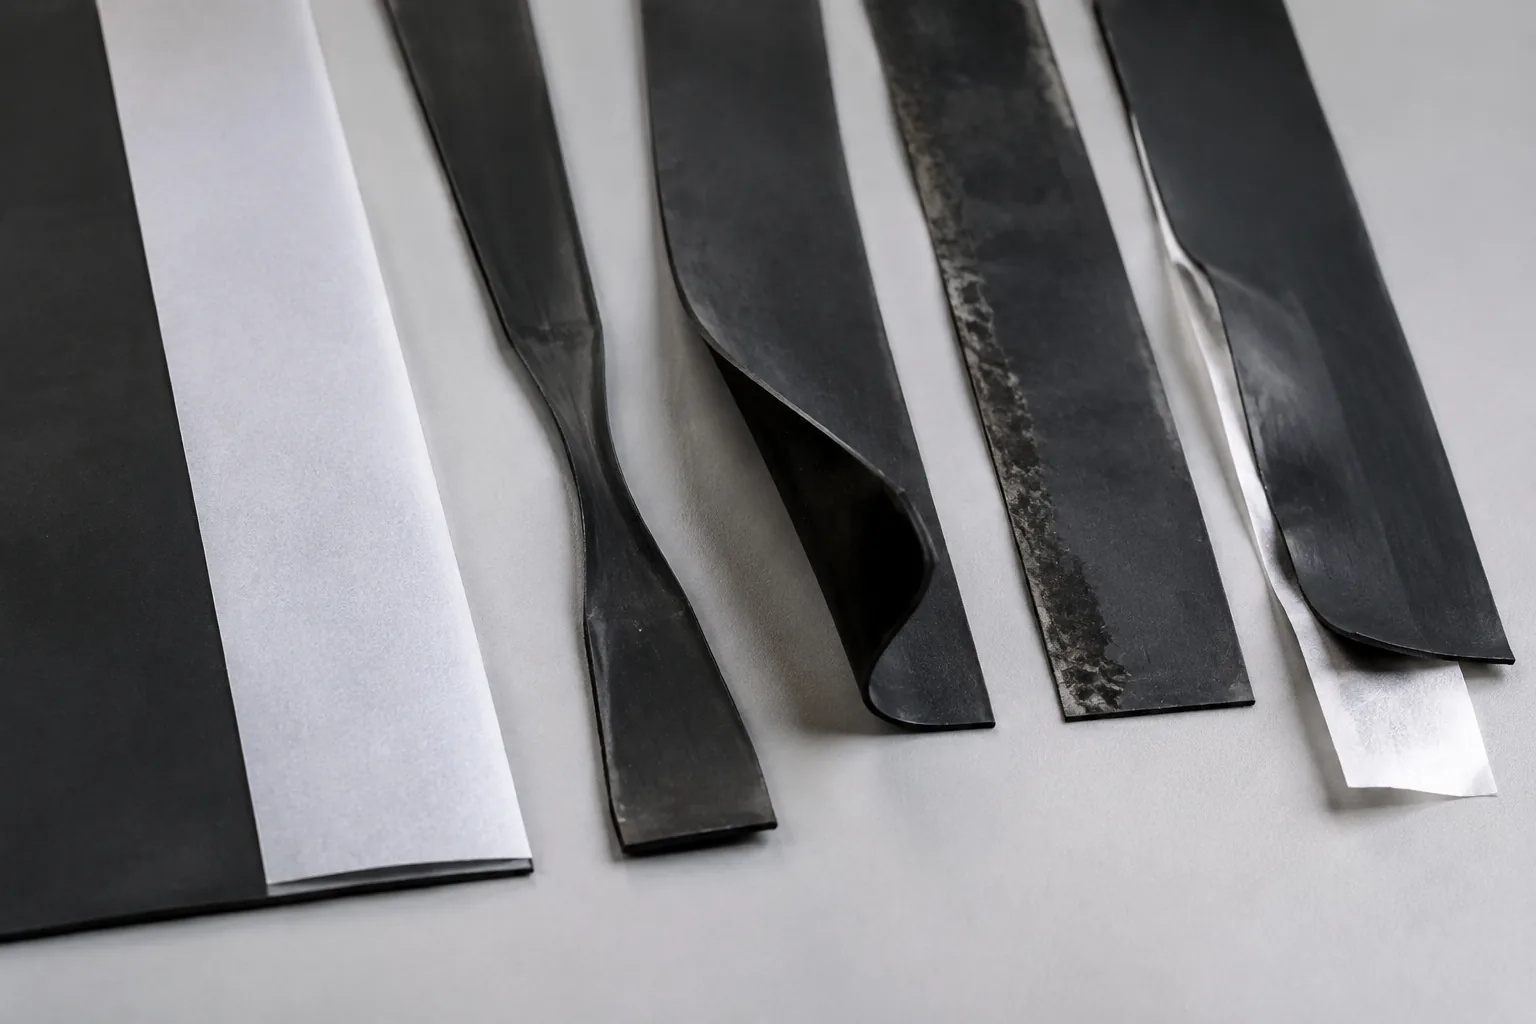
Rubber, Tires & Gaskets
Slitting Calendered Tire Innerliner Rubber Sheet
Technical guidance for slitting tacky calendered tire innerliner sheet while controlling width, edge stretch, liner tracking and rubber deposits.
Read the application guide →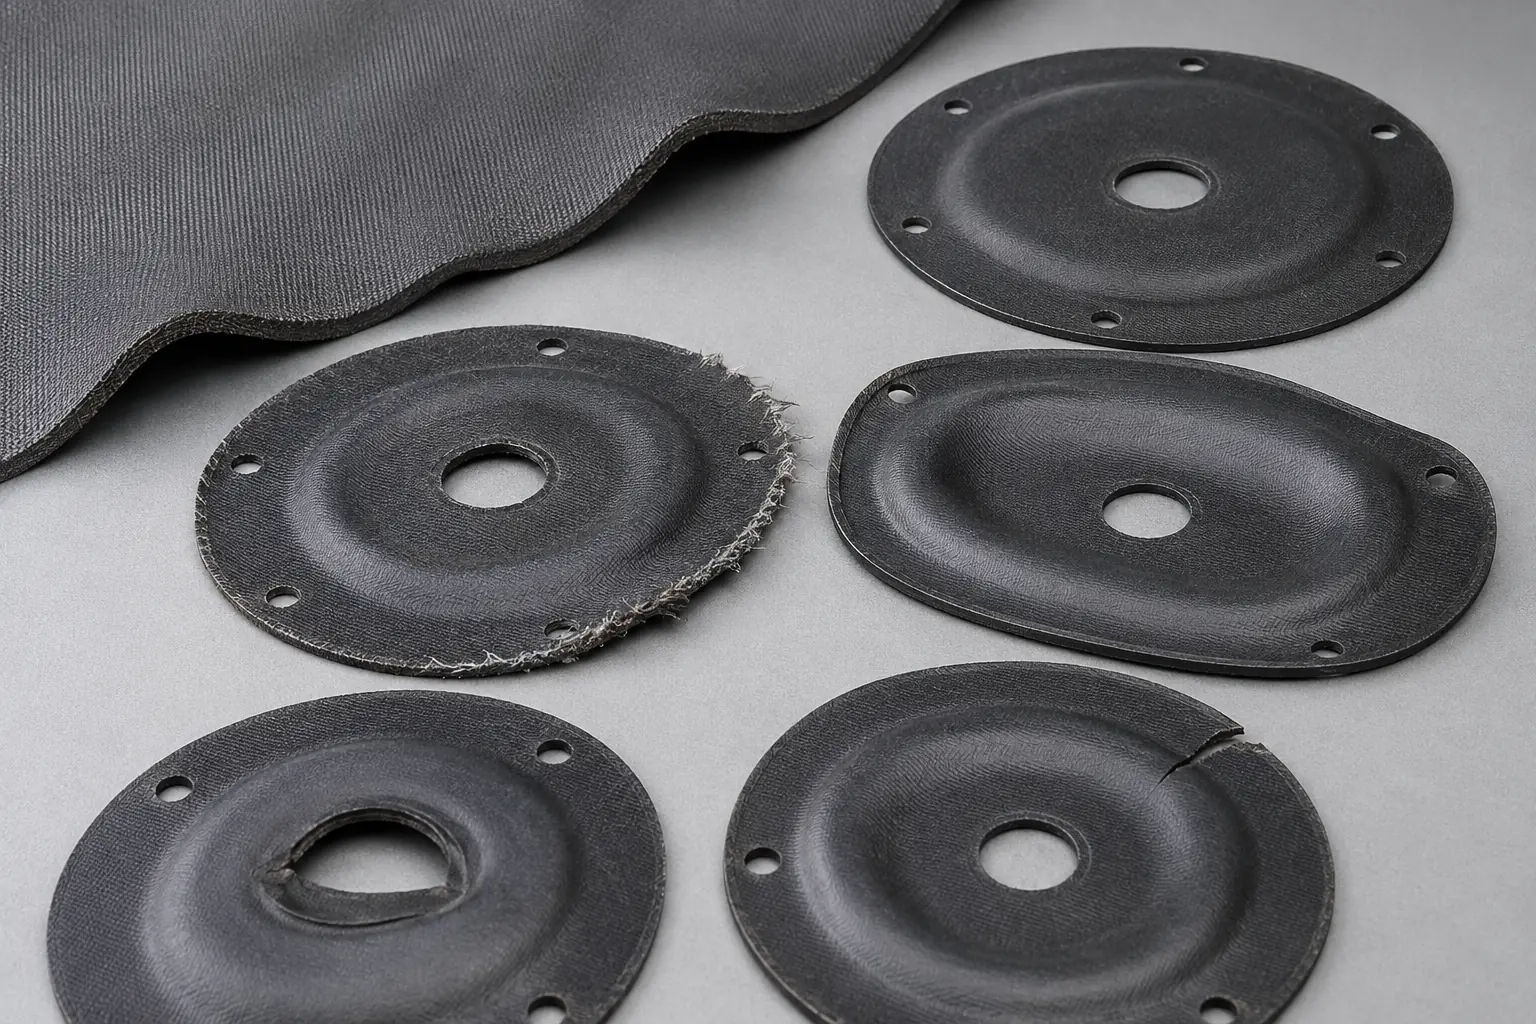
Rubber, Tires & Gaskets
Rubber Diaphragm Blank and Profile Cutting
Guidance for cutting reinforced rubber diaphragm blanks and profiles while protecting fabric orientation, sealing edges, thin flex zones and dimensions.
Read the application guide →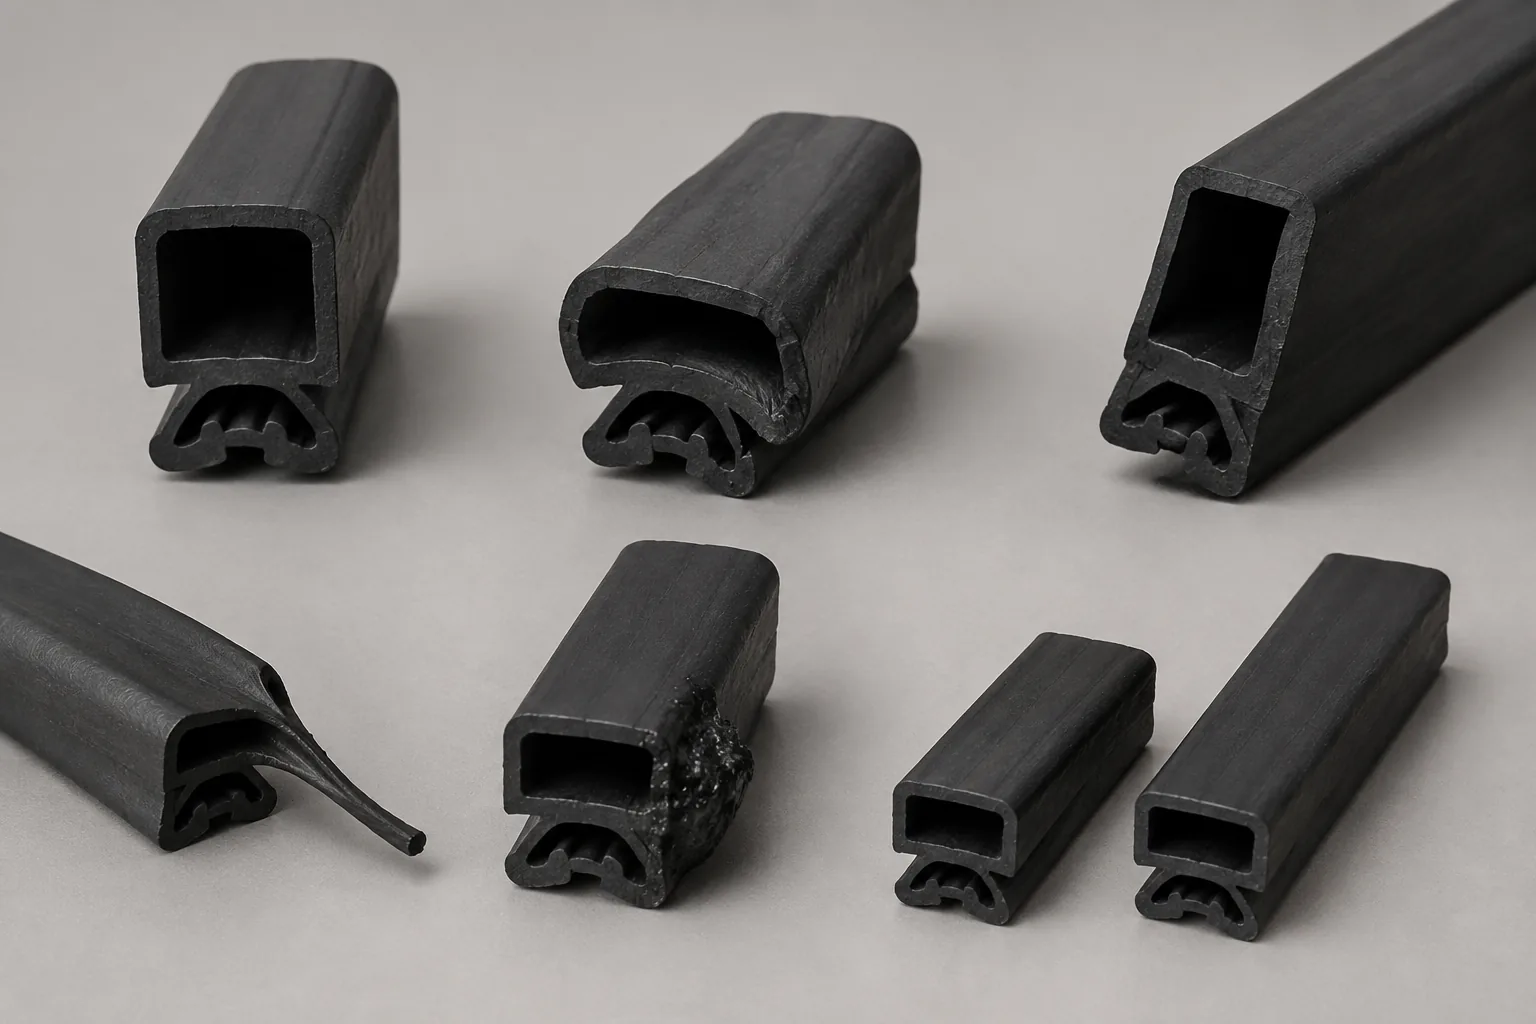
Rubber, Tires & Gaskets
Cutting Extruded Rubber Profiles to Length
Technical guidance for in-line cutoff of extruded rubber profiles, including support of hollow sections, end-face squareness, stretch and edge deposits.
Read the application guide →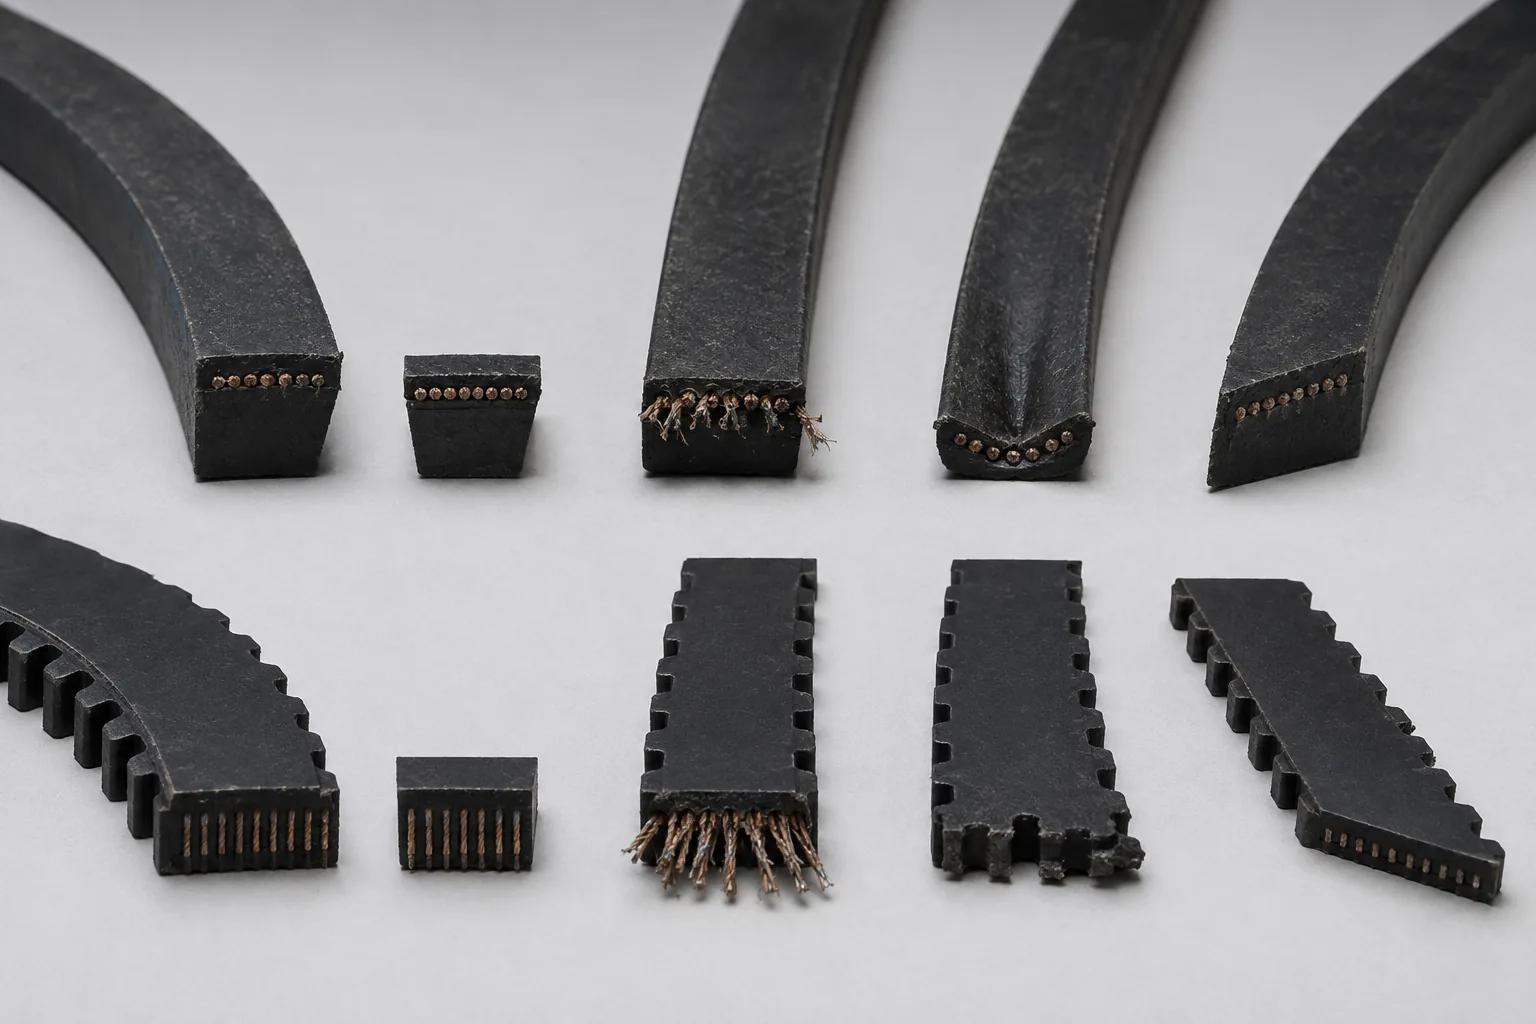
Rubber, Tires & Gaskets
V-Belt and Timing Belt Cut-to-Length Processing
Technical guidance for cutting V-belts and timing belts to length while controlling tensile-cord fray, tooth damage, end angle and section distortion.
Read the application guide →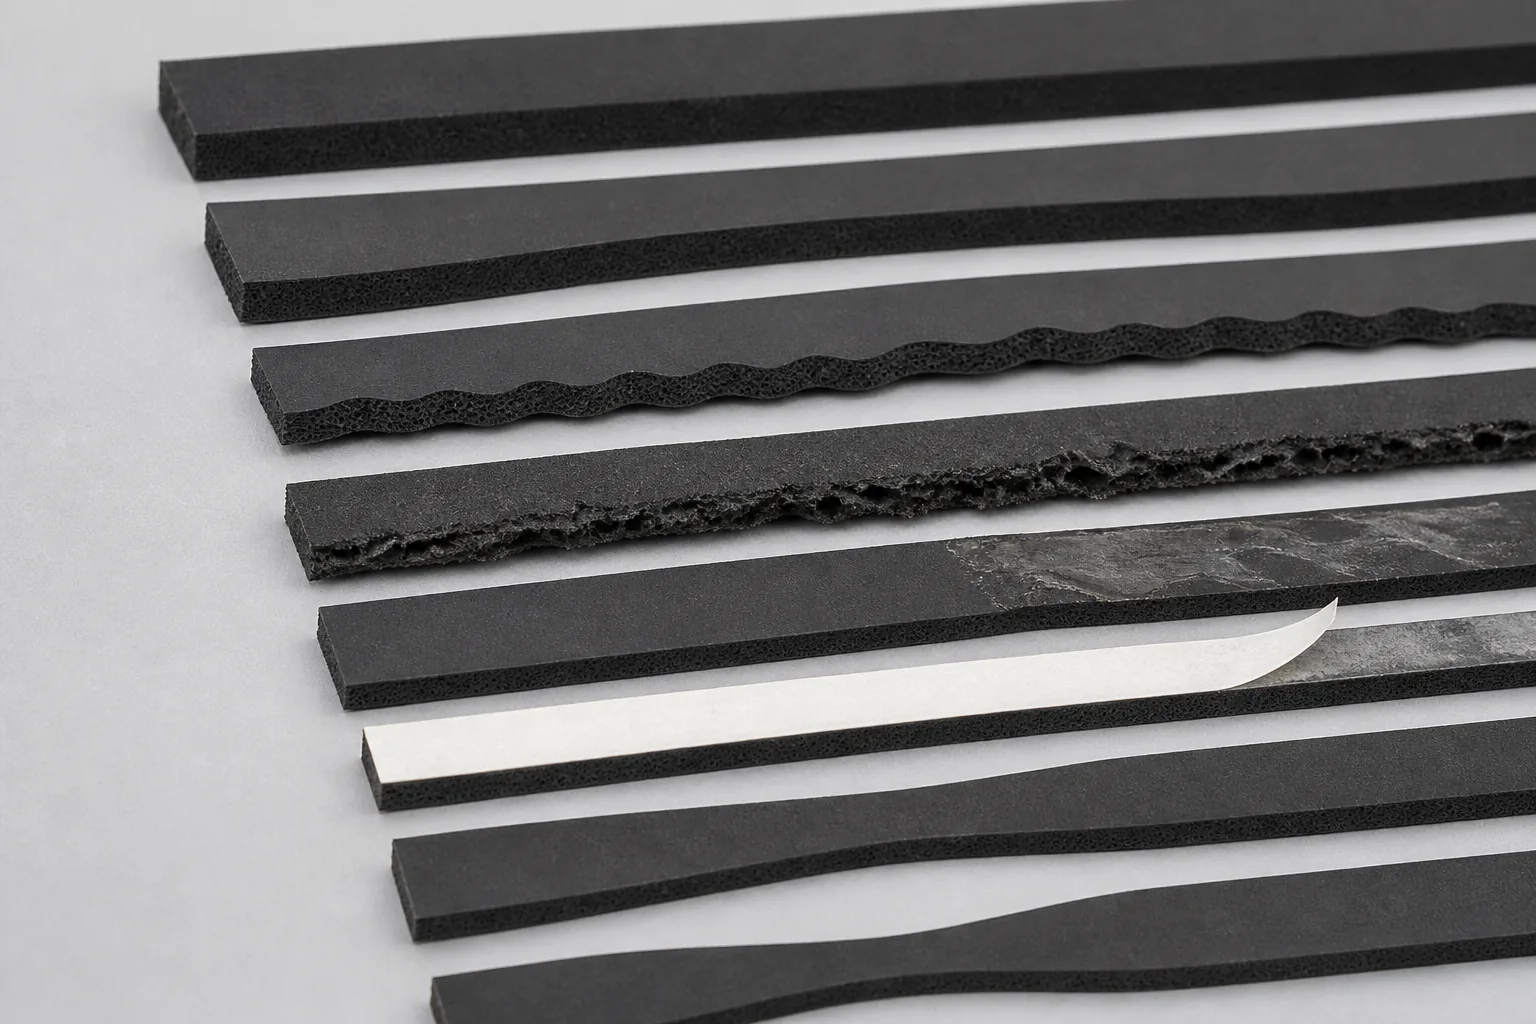
Rubber, Tires & Gaskets
Slitting Sponge Rubber and Elastomer Foam
Guidance for slitting sponge rubber and elastomer foam sheet without crushing cells, wandering off width, tearing the surface or transferring adhesive.
Read the application guide →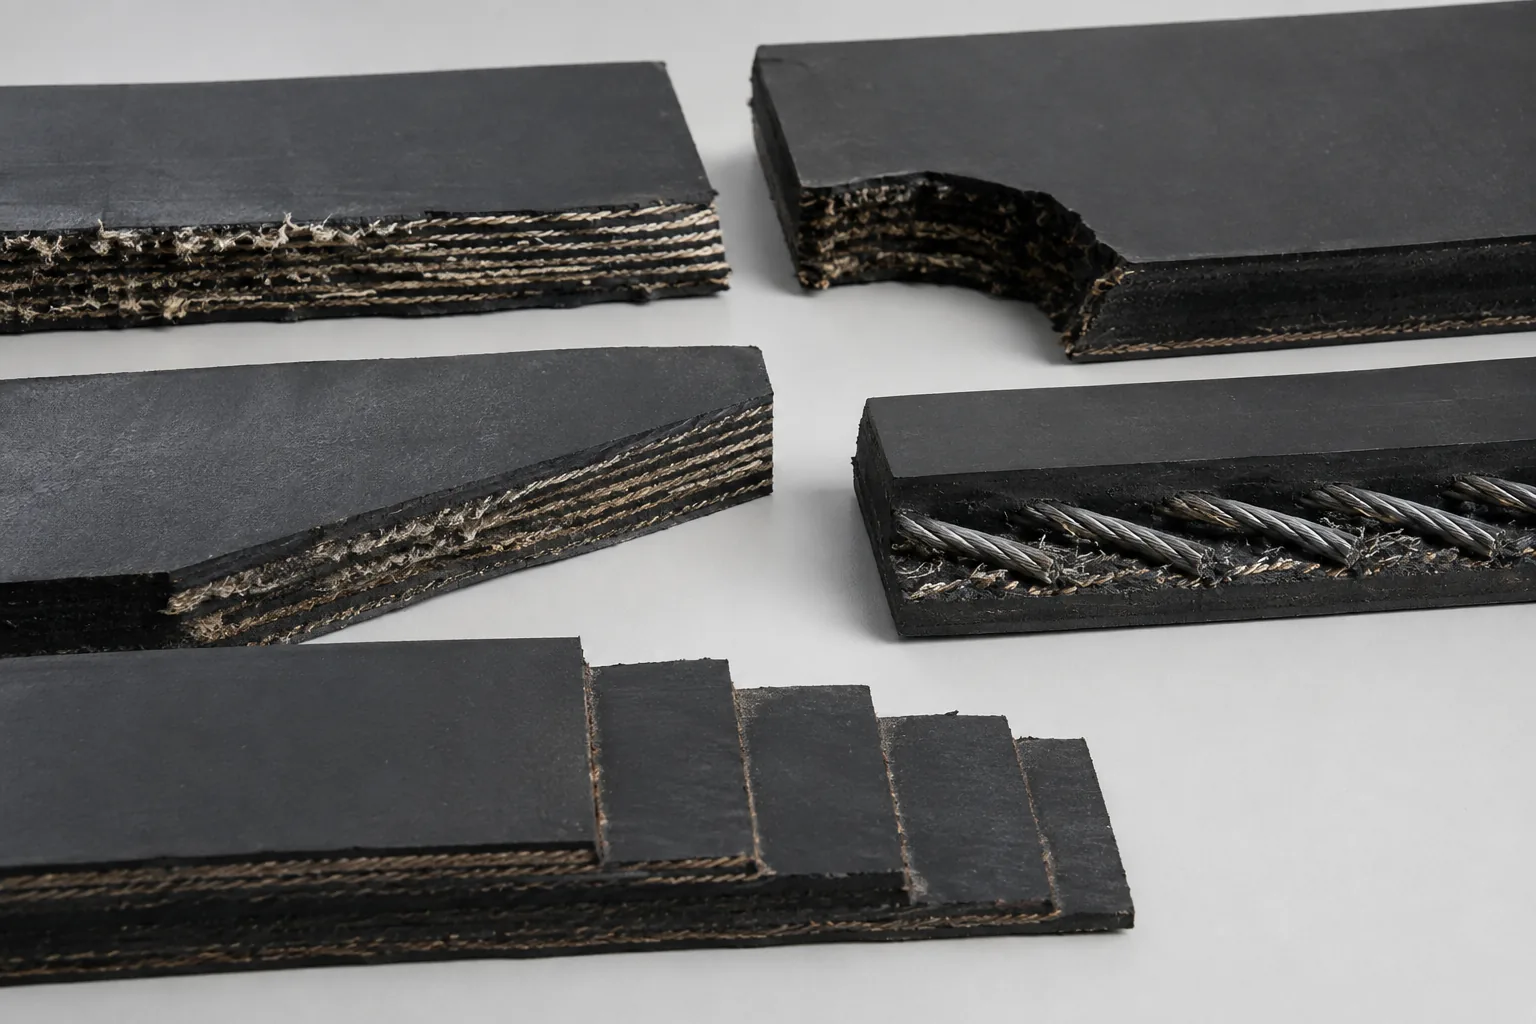
Rubber, Tires & Gaskets
Trimming Rubber Conveyor Belt Edges
Technical guidance for trimming reinforced rubber conveyor belts, focusing on ply fray, thick-section cut drift, rubber chunking and end preparation.
Read the application guide →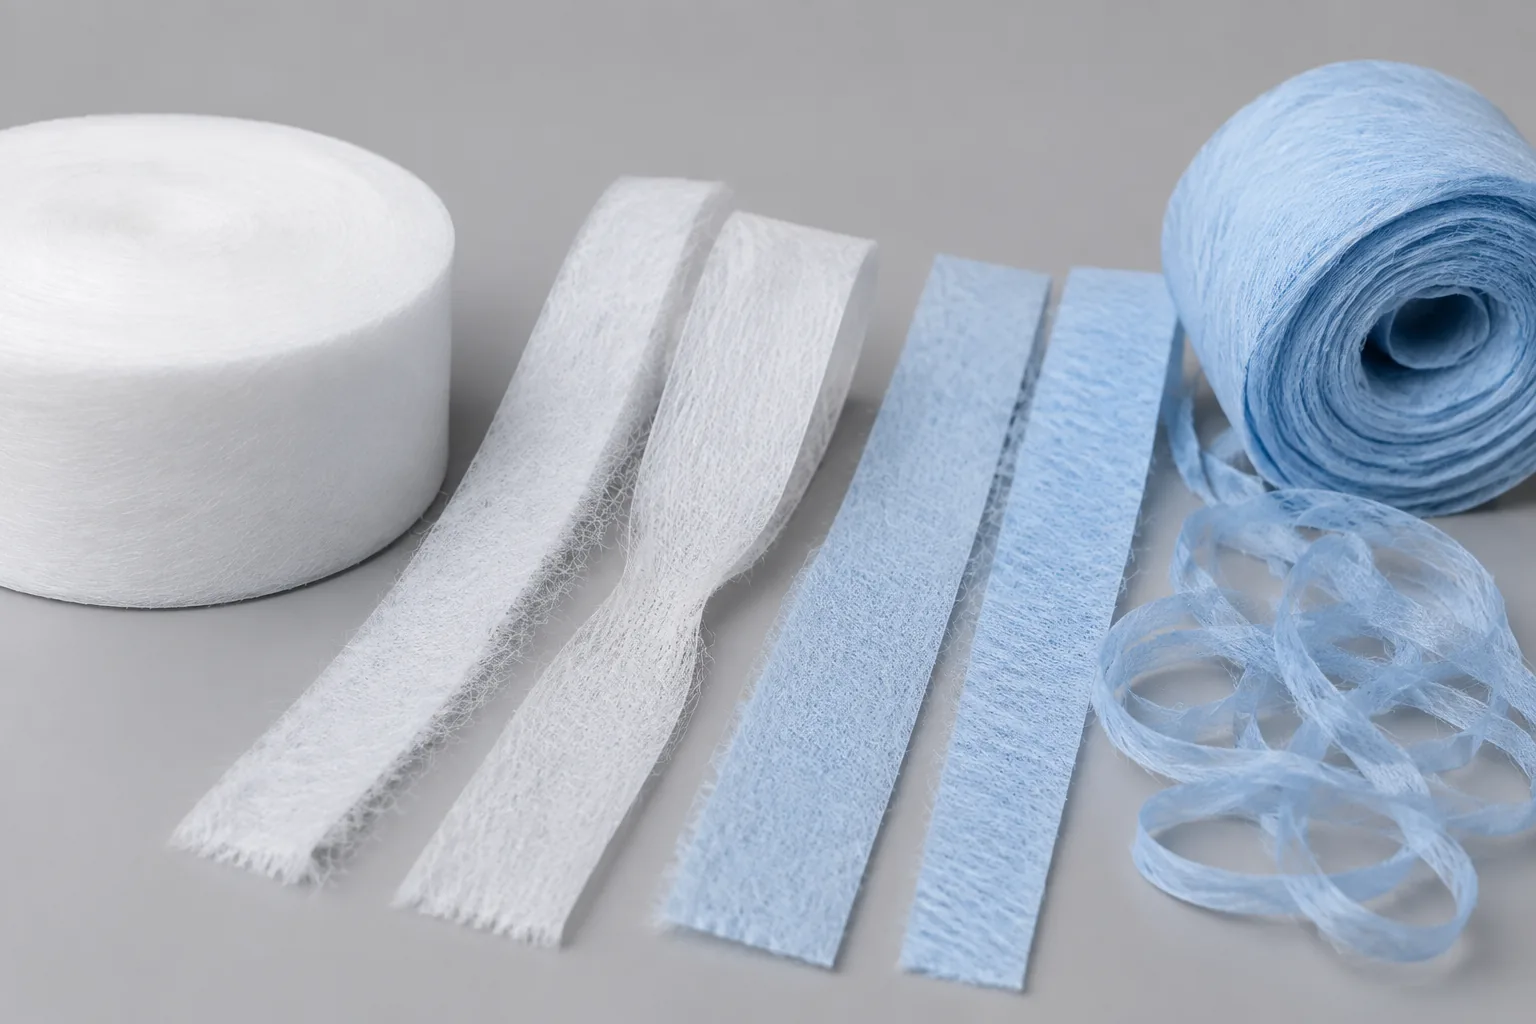
Films & Foils
Slitting Spunbond Nonwoven Rolls
Guide to slitting spunbond nonwoven rolls with stable web tracking, low lint, clean fiber separation and repeatable finished-roll width.
Read the application guide →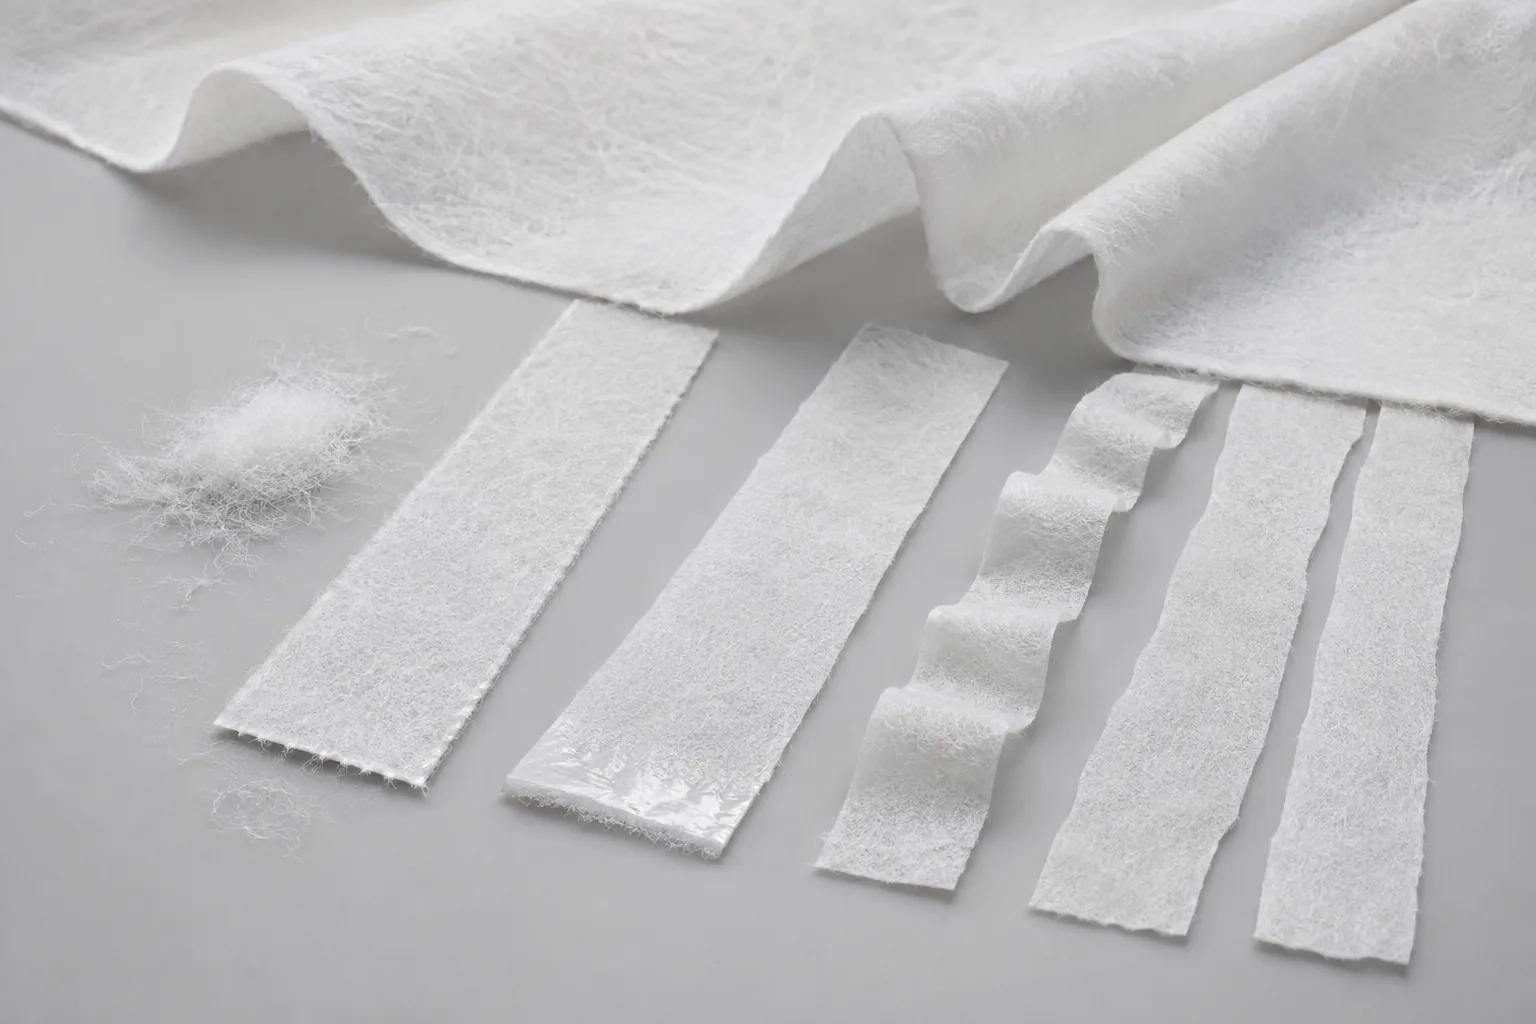
Films & Foils
Slitting Meltblown Nonwoven Web
Application guidance for precision slitting meltblown filtration web while controlling fiber shedding, thermal edge damage, flutter and slit width.
Read the application guide →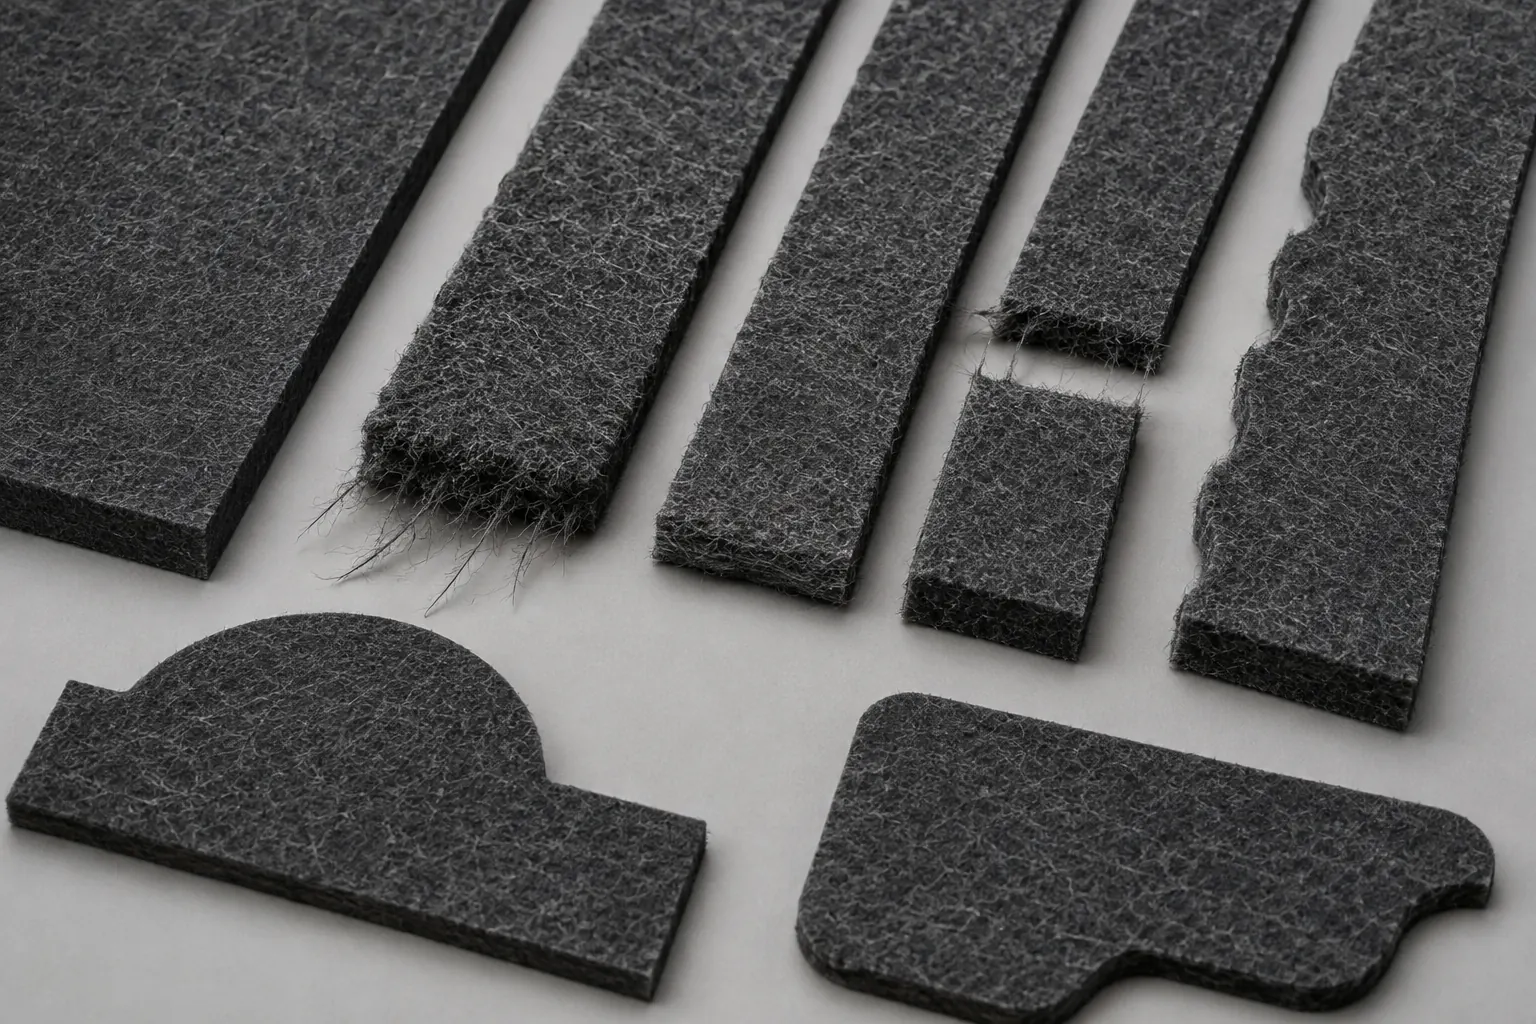
Films & Foils
Cutting Needle-Punched Felt
Technical guidance for cutting needle-punched felt, including dense-fiber separation, edge compression, incomplete cuts and contour tracking.
Read the application guide →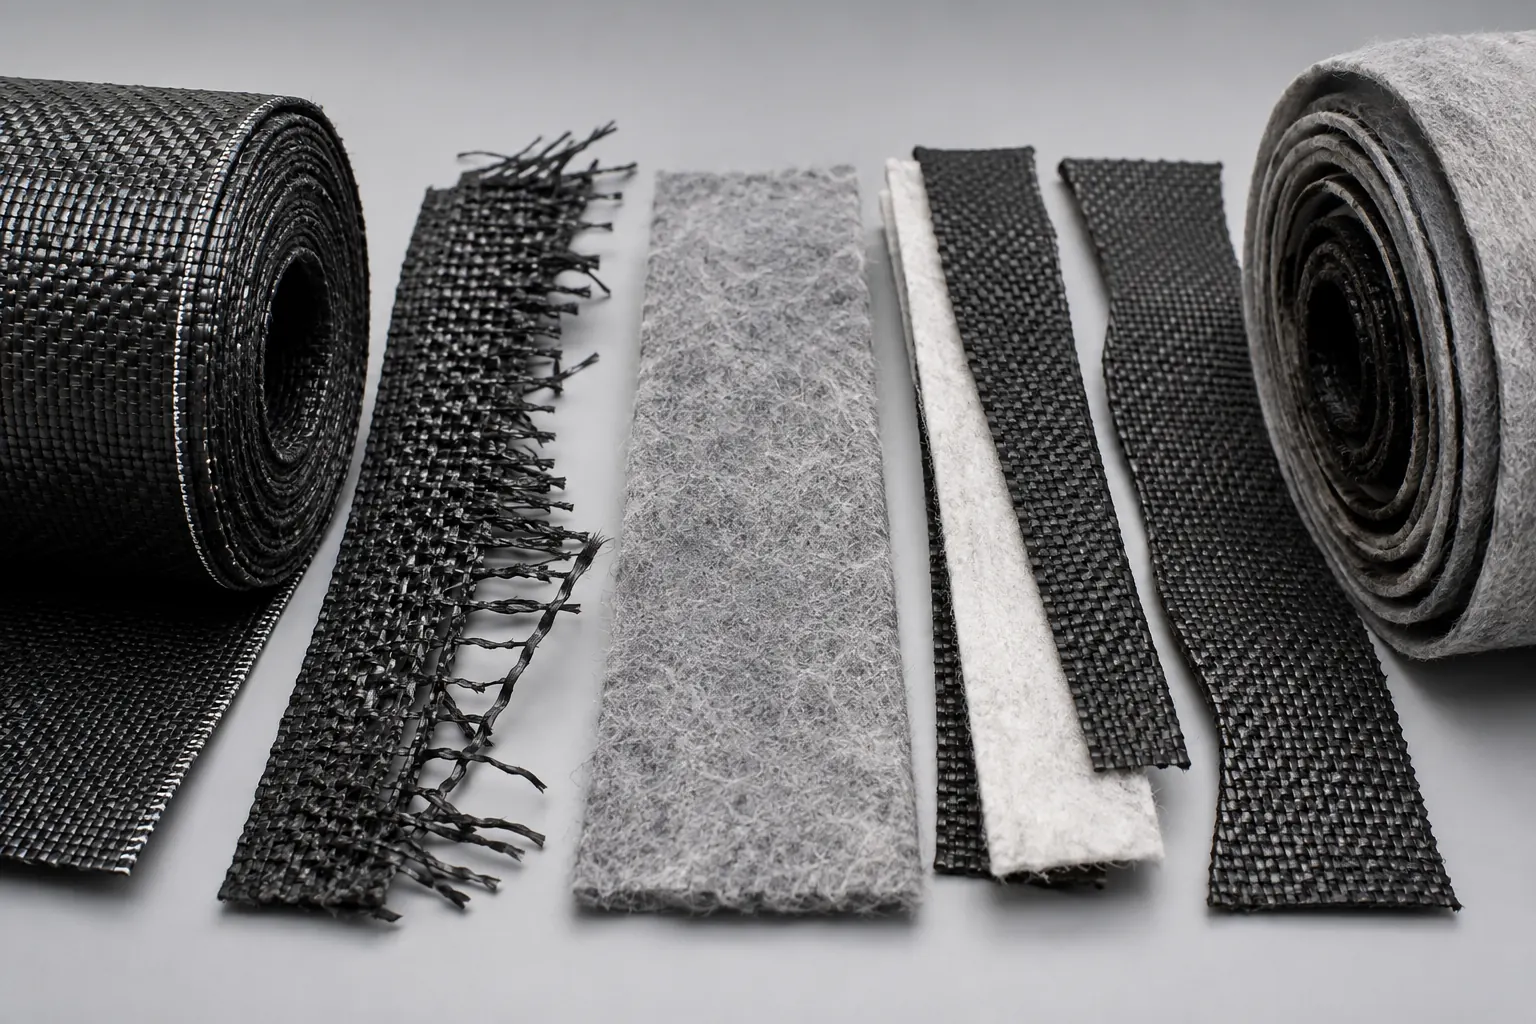
Films & Foils
Slitting Geotextile Rolls
Technical guidance for slitting woven and nonwoven geotextile rolls while managing edge fray, layer movement, width control and heat buildup.
Read the application guide →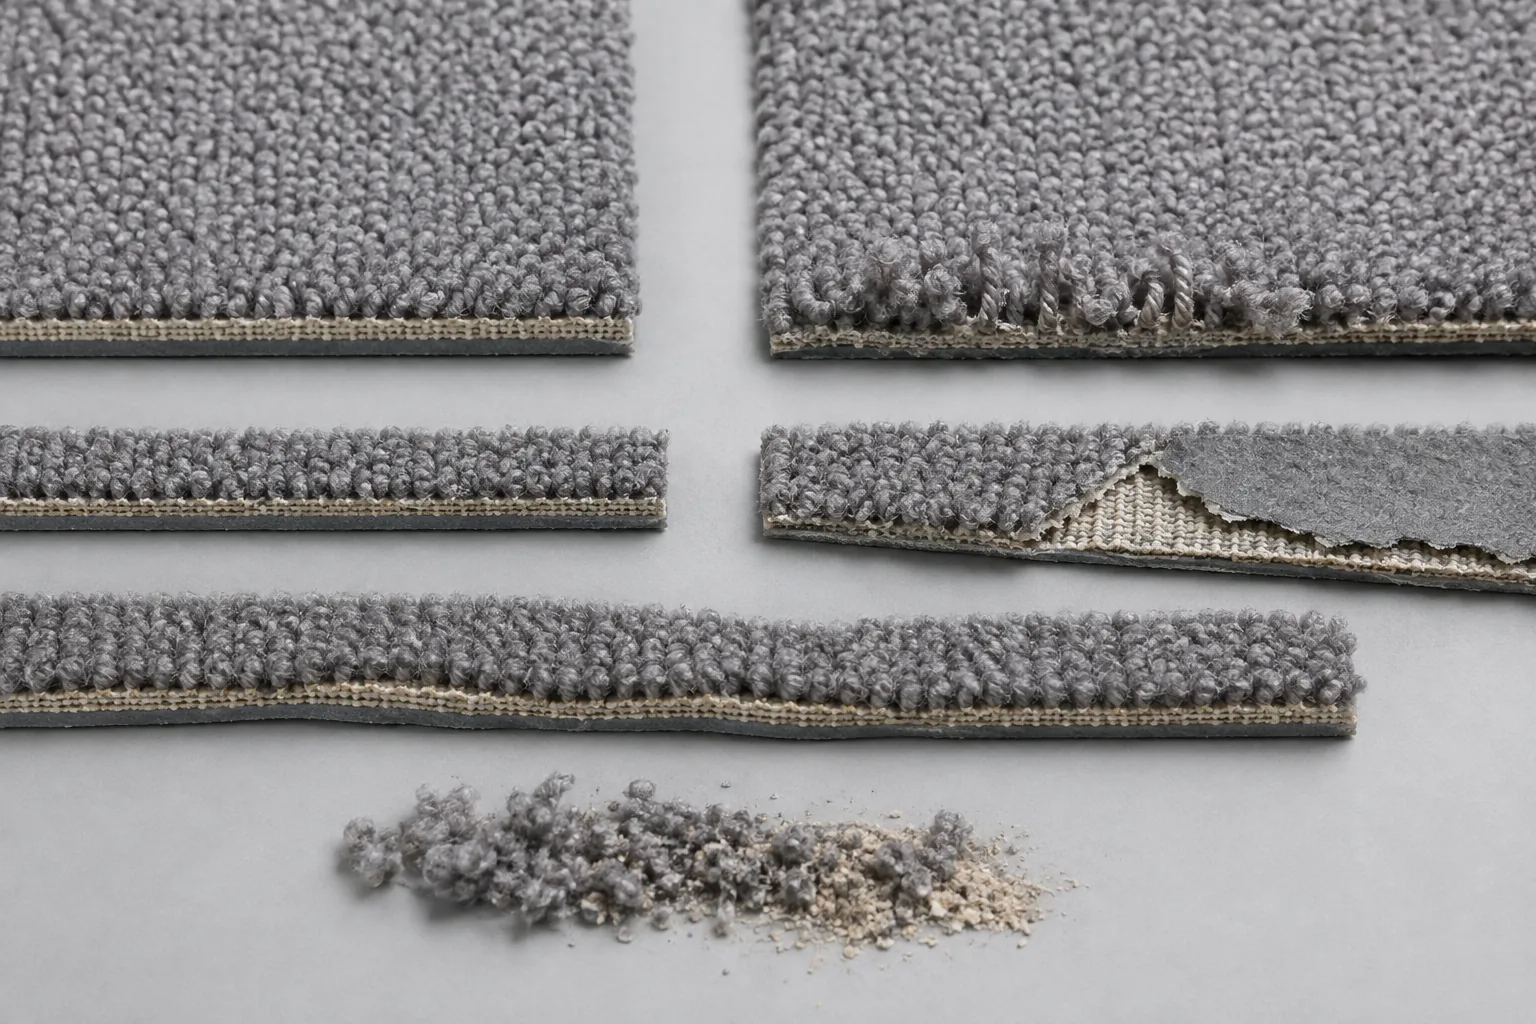
Films & Foils
Trimming Tufted Carpet Roll Edges
Guidance for trimming tufted carpet rolls with controlled pile, backing and edge geometry while reducing yarn pullout, drift and fiber buildup.
Read the application guide →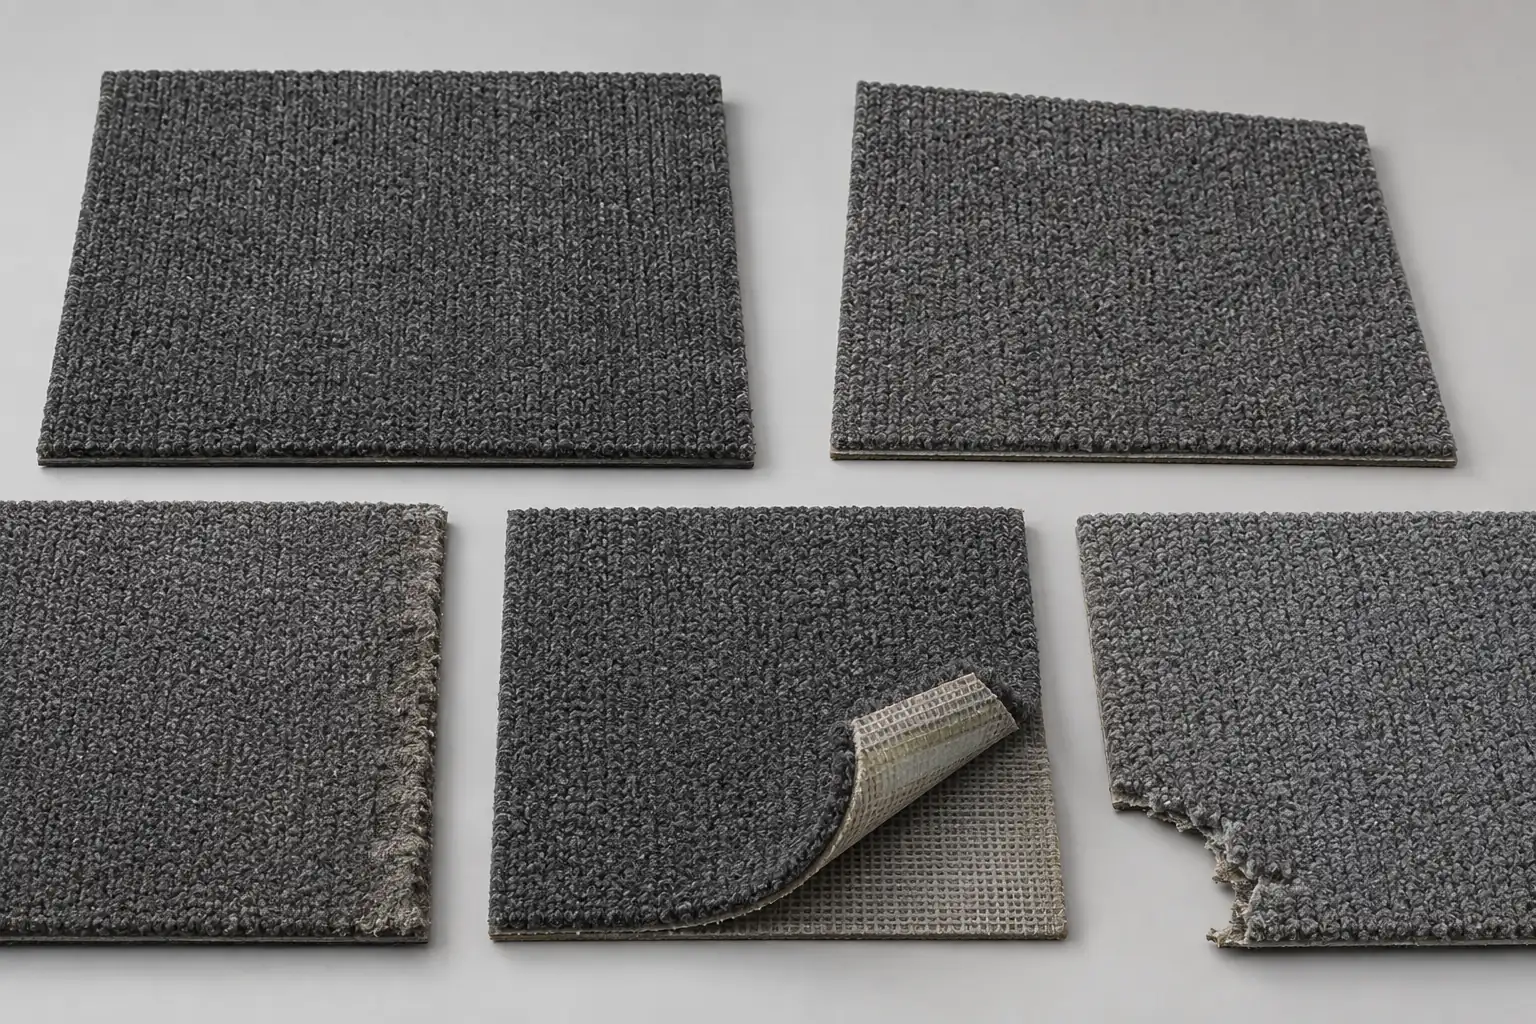
Films & Foils
Cutting Carpet Tiles to Size
Technical guidance for sizing carpet tiles while protecting pile and backing, controlling squareness and preventing corner damage or delamination.
Read the application guide →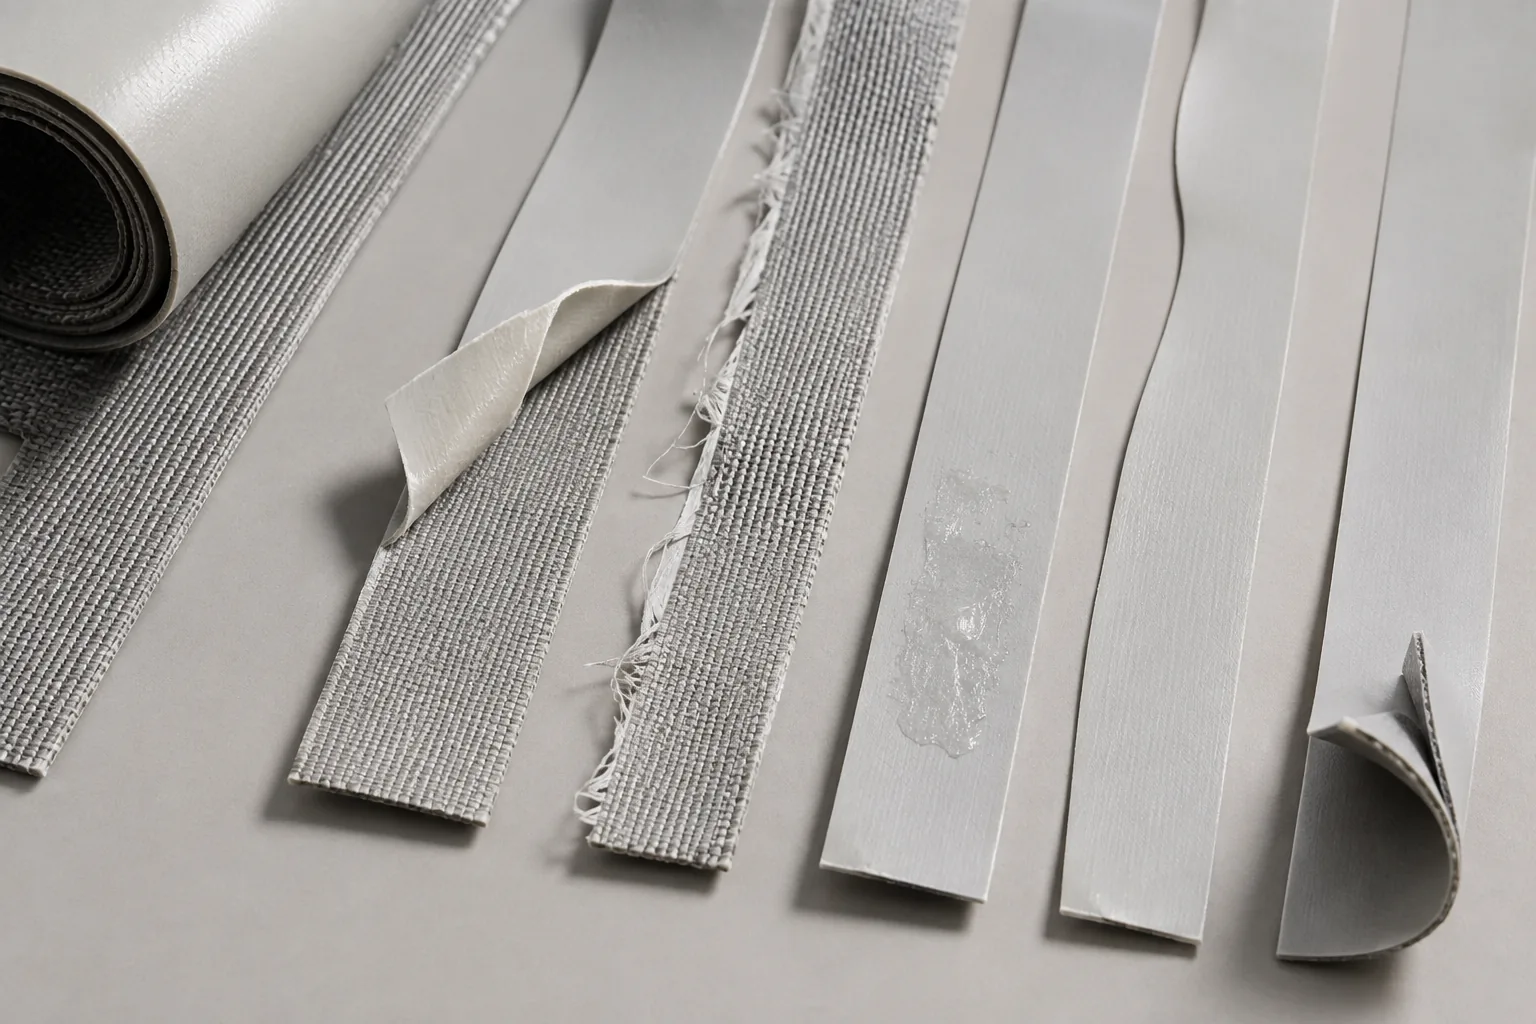
Films & Foils
Slitting Coated Technical Fabrics
Guidance for slitting coated technical fabrics while controlling coating peel, textile fray, tacky residue and lateral movement of the web.
Read the application guide →
Films & Foils
Trimming Nonwoven Filter Media Rolls
Technical guidance for trimming nonwoven filter media rolls with low particle release, controlled pore-layer compression and stable web width.
Read the application guide →
Films & Foils
Chopping Synthetic Staple Fiber Tow
Guidance for chopping synthetic staple-fiber tow to uniform length while preventing fused bundles, uncut filaments, wrap and excessive short fiber.
Read the application guide →
Films & Foils
Cross-Cutting Woven Industrial Fabric
Technical guidance for cross-cutting woven industrial fabric while controlling weft distortion, fray, ply movement and incomplete edge separation.
Read the application guide →
Films & Foils
Cutting Braided and Twisted Textile Cord
Guidance for cutting braided and twisted textile cord to length while limiting strand splay, flattened ends, partial filament cuts and variation.
Read the application guide →
Films & Foils
Sheeting Nonwoven Wipe Material
Technical guidance for sheeting nonwoven wipe material with stable length, low lint, complete edge separation and controlled folded-web handling.
Read the application guide →
Films & Foils
Slitting Flexible Plastic Film Rolls
Guidance for high-speed slitting flexible plastic film while controlling stretch, wrinkles, static movement, edge curl and finished-roll width.
Read the application guide →
Films & Foils
Trimming PET Sheet Edges
Technical guidance for trimming PET sheet while controlling stress whitening, brittle edge cracks, plastic burrs and finished-width variation.
Read the application guide →
Packaging & Paper
Cutting Extruded Plastic Pipe to Length
Guidance for cutting rigid plastic pipe in line while limiting melt, bore burr, ovalization and angled end faces across pipe sizes.
Read the application guide →Industrial Blade Application Guides: From Material to Cutting Edge
Reliable cutting comes from a system, not a single hardness number. Industrial blade technology connects the processed material, cutting method, machine condition, blade material, heat treatment, geometry, grinding accuracy and maintenance practice.
This page gives engineers and buyers a practical framework for discussing blade performance with Meirente before a quotation, trial or repeat-order improvement.
Start With the Cutting Application
A thin film, abrasive glass fiber, soft food product, polymer strand and electronic ceramic sheet place very different demands on a blade. The first questions should cover material behavior, thickness, speed, cutting gap, temperature, contamination, target finish and the cost of downtime.
Material Selection Is a Balance
Tool steel, stainless steel, high-speed steel, powder-metallurgy grades, tungsten carbide and coated solutions offer different combinations of hardness, toughness, wear resistance, corrosion resistance and cost. Selection should reflect the dominant failure risk instead of using the same grade for every application.
Edge Geometry Controls How the Blade Enters the Material
Bevel angle, single- or double-bevel direction, edge thickness, tooth pitch, tooth height, rake and clearance influence cutting force, dust, burrs, heat and edge strength. A sharper edge can reduce force, but an edge that is too thin may chip or deform under impact.
Heat Treatment, Grinding and Surface Engineering
Heat treatment develops the material properties required by the design. Precision grinding then controls flatness, parallelism, runout, concentricity and final edge geometry. Surface finishing or coating may help with wear, friction, corrosion or material adhesion when the application and base material justify it.
Measurement and Failure Feedback
Inspection confirms whether the blade matches the agreed specification; production feedback confirms whether the specification matches the real process. Photos and records of wear, chipping, deformation, burrs, dust, motor load, heat and cutting hours help separate material problems from alignment, gap, vibration or contamination issues.
Is higher hardness always better?
No. Higher hardness can improve wear resistance but may reduce toughness. The correct balance depends on impact, material abrasiveness and machine stability.
Why does the same blade wear differently on two machines?
Alignment, holder condition, cutting gap, speed, cooling, vibration, contamination and processed material can all change blade life.
When should a coating be considered?
Consider it when wear, friction, corrosion or adhesion is a defined problem and the coating is compatible with the base material, edge and operating temperature.
What information helps diagnose chipping?
Provide the chipped location, installation direction, holder condition, cutting gap, speed, processed material, contamination risk and close-up photos.
Can edge geometry be changed without changing the machine?
Sometimes, but the blade-holder interface, clearance and cutting method must be reviewed before any geometry change is approved.