
Blade Application Guides / Application Guide / Specialty metal converting
Tantalum Metal Foil Strip Edge-Trimming Blades
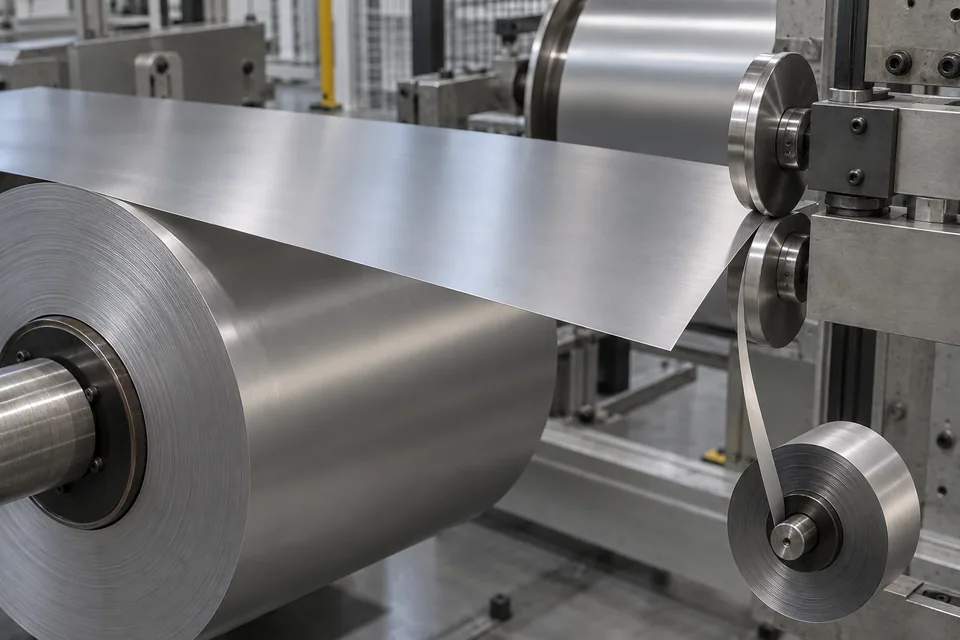
Admat supplies tantalum strip and foil on coils, and Ulbrich describes edge condition and scrap control as part of metal-foil slitting. A strip edge-trimming pass removes a documented longitudinal margin from a retained tantalum web. It is narrower in scope than making several new coils and separate from crosscutting sheets. The reason may be a damaged edge or a specified final width, but the amount removed must be authorized by the downstream drawing. Tantalum grade, temper and foil gauge matter to burr and edge curl; the resulting strip must feed the next operation.
Updated
Where This Cutting Application Appears
Map the outside margin
Measure incoming width and locate the defect or sacrificial mill edge. Confirm minimum retained width for a later drawn cup, stamped shield or other part. Identify whether one or both edges are to be trimmed and how rolling direction must be maintained. If a flaw lies inside the permitted trim line, seek disposition instead of cutting deeper without approval.
Stabilize waste takeoff
Support the web near the outside cut and arrange a path for the narrow tantalum ribbon. Scrap can curl back toward the retained edge or mark the broad face. Trial a blade arrangement on the actual foil gauge and condition, noting which side develops the exit burr. Protect the coil from guide scratches.
Inspect the retained strip
Measure width and straightness at multiple positions. Examine the fresh edge for burr, rollover, tearing, waviness and fine slivers. Check the untouched side too, since a misaligned guide can damage it. Compare relaxed strip samples with the wound face to detect edge curl or camber that a single flat piece may hide.
Keep the material identity
Record tantalum grade, processing route, lot, trimmed side and scrap width. Use buyer-approved packaging and interleave to avoid surface contamination. A trimmed strip with a sound edge but unknown metal route may be unsuitable for a specified later forming process.
Run the next feeder
Unwind a representative retained coil through the intended stamping or sheet-feeding route. Check whether the fresh edge tracks without snagging and whether useful width remains for the component. Reinspect after the feed trial. The edge-trimming result cannot by itself establish final part formability or corrosion performance. Before approving a recovered coil, compare actual edge condition with the drawing’s connection or forming zone. A burr outside the functional land may have a different disposition from one that enters a later weld, but the buyer sets that distinction. Preserve the incoming edge sample.
Define the Required Cut Result
- Remove an authorized tantalum edge margin.
- Maintain the drawing-required usable width.
- Limit burr, slivers, curl and scrap entanglement.
- Keep grade and processing-route traceability.
Problems to Diagnose Before Changing the Knife
Narrow waste ribbon wraps the tool
- Improve scrap routing.
- Check knife contact.
- Stop before retained foil is pulled.
Trimmed coil develops camber
- Review side loading and web guides.
- Measure after relaxation.
- Trial downstream feed.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Guided edge-trim shear | For a supported tantalum foil web. | Verify burr direction and width. |
| Paired circular trim knives | Where the installed coil line supports the specified gauge. | Check both faces and waste control. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Tantalum grade and foil gauge
- Incoming and minimum retained width
- Damaged side or specified edge waste
- Winding and scrap route
- Burr, curl and feed acceptance
Questions About This Cutting Application
Is edge trimming a multi-lane slit?
No. It removes a narrow outside ribbon and keeps the main strip.
May a defect be trimmed away at any cost?
No. The retained width must still meet the drawing.
Why record which edge was cut?
Burr direction and downstream orientation can matter.
Does a clean trim prove formability?
No. The later drawn or stamped part must be tested.
Public references and scope
These public sources provide material, cutting-method or safety context for this guide. Supplier pages describe their own materials or equipment; they do not establish a MEIRENTE blade specification or performance claim. Confirm the actual grade, machine setup and required cut with a drawing or sample.
Related product and service information
- Cotton Pad and Cosmetic Round Cutting - cotton pads and cosmetic rounds · stack cutting and shaping
- Amorphous Metal Ribbon Strip Edge-Trimming Blades - amorphous metal ribbon · strip edge trimming
- Nanocrystalline-Alloy Precursor Ribbon Strip Edge-Trimming Blades - nanocrystalline-alloy amorphous precursor ribbon · strip edge trimming
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.