
Blade Application Guides / Application Guide / Specialty metal converting
Nanocrystalline-Alloy Precursor Ribbon Strip Edge-Trimming Blades
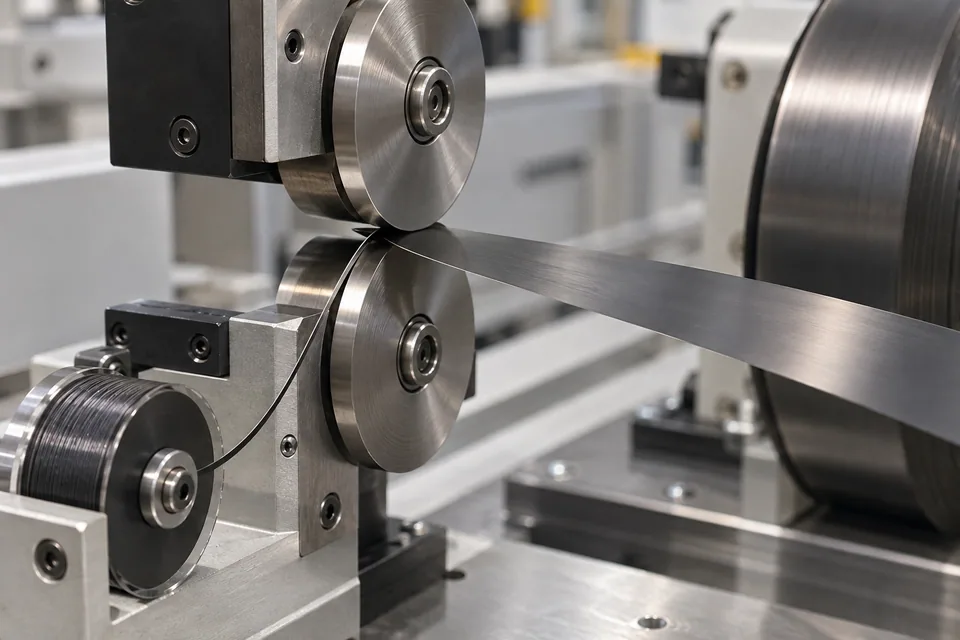
Metglas describes a wide, fully amorphous FT-3W precursor that can be slit into narrower strands and later heat-treated. Its data distinguish samples near the cast-width edges and center. Proterial’s FINEMET sequence confirms that the feedstock remains amorphous until the subsequent core heat treatment. A separate edge-trim pass is therefore a conditional conversion step for a documented casting-edge flaw or released useful-width boundary, not a routine treatment for every precursor roll. This guide removes a narrow margin from one side of the still-unannealed ribbon and collects it as waste. DIENES describes paired shear cutting of continuous foil webs, but the actual alloy, cast texture and fragile trim width need a representative trial. No visual edge check replaces post-anneal core testing.
Updated
Where This Cutting Application Appears
Map the casting edge before cutting
Identify whether defects occur on the wheel side, free side or outer margin and measure how far they enter the proposed retained width. Record coil position for chips, ripples and width loss. A fixed trim line cannot rescue a crack that extends farther into the core-width lane.
Design a single-side trim station
Use one controlled shear pair on the specified waste edge. Establish guide reference and waste takeoff so the retained ribbon remains wide enough for the core maker. Inspect whether the thin scrap strand runs continuously or breaks and scatters fragments near the product reel.
Compare old and new edge specimens
Retain samples before and after trimming, marked by source-coil position. Look for fresh notches, raised lip and loose metallic flakes under magnification. Check width and flatness over the reel; an attractive new edge is still a failure if useful width falls below drawing.
Trial the retained ribbon in core winding
Rewind without adding edge damage, then let the buyer form a representative core and perform the intended anneal. Compare mechanical yield and finished magnetic tests with an untrimmed control where appropriate. The trim decision should reflect the full build, not a single micrograph.
Define the Required Cut Result
- Remove only a documented unusable cast margin.
- Preserve core-useful width and continuous winding behavior.
- Keep broken trim fragments out of the product reel.
- Retain before/after evidence for material disposition.
Problems to Diagnose Before Changing the Knife
New edge develops a fine crack line
- Inspect shear engagement and knife condition.
- Compare original cast-edge samples from the same position.
Waste strand breaks repeatedly
- Review waste width, takeoff tension and incoming cracks.
- Inspect reels for loose fragments.
Retained reel is too narrow
- Check guide position and source-width variation.
- Sample beyond setup and near reel end.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Single paired rotary shear at the defective edge | Only when the casting flaw lies outside the retained core width on unannealed stock. | Confirm continuous waste, no fresh chips and winding yield. |
| No trim or supplier replacement | If the source coil meets drawing or cracks cross the proposed boundary. | Use buyer-approved material disposition rather than an unsupported extra cut. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Precursor alloy and casting/heat history
- Defect-depth map and affected edge
- Minimum useful width after trim
- Wheel/free side and unwind direction
- Shear engagement and guide reference
- Waste takeoff and fragment containment
- Before/after edge acceptance method
- Core winding, anneal and magnetic test owner
Questions About This Cutting Application
Is this a trim of an annealed nanocrystalline core?
No. The web remains a loose, unannealed amorphous precursor.
Why not trim every cast edge?
A sound as-cast edge may be usable and another cut adds risk.
Can one trim remove cracks inside the finished width?
No. Those require material disposition or another approved plan.
Why label where samples came from?
Edge and center positions may differ within a wide cast ribbon.
What is the key RFQ evidence?
Provide the defect map, minimum retained width and precursor lot data.
Public references and scope
These public sources provide material, cutting-method or safety context for this guide. Supplier pages describe their own materials or equipment; they do not establish a MEIRENTE blade specification or performance claim. Confirm the actual grade, machine setup and required cut with a drawing or sample.
Related product and service information
- Niobium Metal Foil Cut-To-Length Blades - niobium metal foil · cut to length
- Amorphous Metal Ribbon Strip Edge-Trimming Blades - amorphous metal ribbon · strip edge trimming
- Beryllium-Copper Foil Strip Edge-Trimming Blades - beryllium-copper foil · strip edge trimming
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.