
Blade Application Guides / Application Guide / Specialty metal converting
Tantalum Metal Foil Precision Coil Slitting Blades
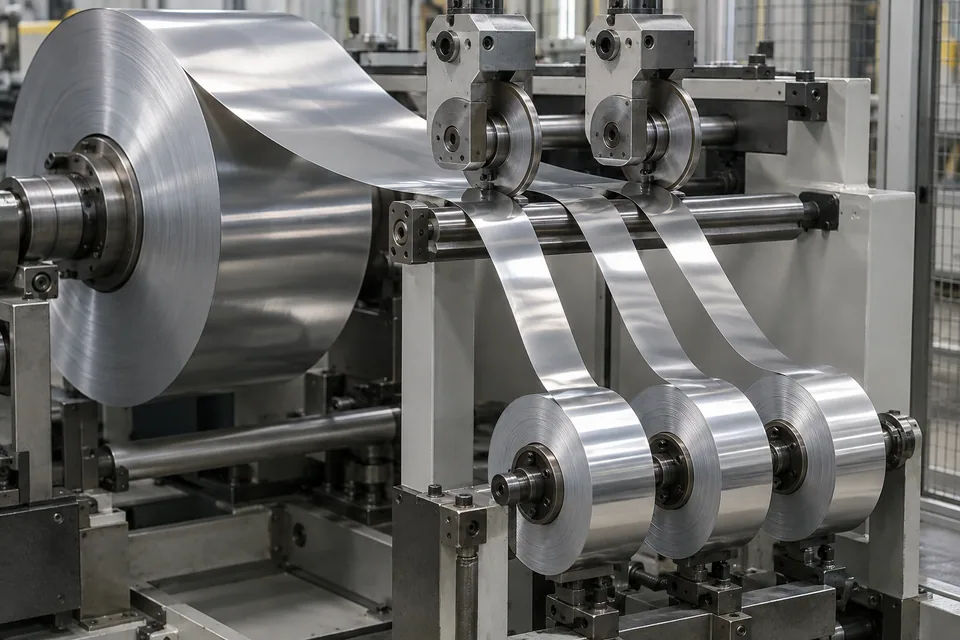
Admat describes precision-rolled tantalum strip and foil supplied as coils for later fabrication; Goodfellow also lists tantalum foil coil stock. Ulbrich documents the general finishing variables of precision metal-foil slitting, including edge condition, winding and interleaving. A tantalum foil slitting job is a longitudinal master-coil conversion, not transverse cut-to-length or part blanking. Because commercial tantalum may be specified in different purity, processing route and temper, tooling must be proven on the actual lot. The narrow coil should be accepted for edge integrity and later feed, not simply nominal width.
Updated
Where This Cutting Application Appears
Define the slit-lane plan
Read the drawing for target widths, coil orientation, edge waste and the intended stamping or forming station. Record whether the order is unalloyed tantalum or an alloy and which production route the supplier used. Admat distinguishes powder-metallurgy and electron-beam material for different forming applications; the converter must not substitute one merely because its width is available.
Prepare the unwind and knives
Keep the foil supported as it leaves the master coil. Set knife spacing and side contact from a representative trial on the specified gauge and condition. Watch for a soft edge that rolls over or a narrow strip that wanders. Avoid using a thick-strip setup as a default for thin foil, since burr and camber can dominate the finished narrow coil.
Inspect cut edges and dimensions
Measure each lane width and inspect both edges for burr, metal slivers, waviness, local tears and tool marks. Check the coil face after winding for telescoping or trapped scrap. Compare start, middle and end samples because knife pickup and web tracking can change through the run.
Preserve surface and lot identity
Label metal grade, processing route, thickness, lot and slit lane. Use only buyer-approved interleaf, core and packaging. Prevent metallic particles or tool lubricants from contaminating foil that may later enter a capacitor, chemical-resistant component or vacuum assembly. Those end uses have different acceptance rules.
Prove downstream feed
Unwind a trial narrow coil in the intended feeder. Look for edge snag, camber and twist that may not appear in a short loose coupon. If the lane will be stamped, inspect its first formed parts before finalizing the slitting setup. The converter’s edge acceptance does not determine the finished component performance. Sample the narrowest lane separately. It is more sensitive to winding tension and side pressure than a wider lane from the same master coil. Record whether the cut edge orientation changes its passage through the receiving guide. Check that the lane label stays legible.
Define the Required Cut Result
- Make stable narrow tantalum foil coils.
- Limit burr, slivers, tears and camber.
- Protect lot, surface and metal condition.
- Verify later feeding and winding.
Problems to Diagnose Before Changing the Knife
Narrow coil telescopes
- Review web alignment and winding tension.
- Check lane camber and core fit.
- Inspect after unwind.
Foil edge rolls over
- Review knife contact and backing.
- Compare both edge faces.
- Inspect later stamping feed.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Precision upper/lower coil-slitting knives | For qualified tantalum foil master coils. | Confirm width, burr and full-length winding. |
| Narrow-lane trim pair | For outside waste lanes where authorized. | Keep scrap separate from retained coils. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Tantalum grade, purity and production route
- Foil gauge, temper and incoming coil size
- Lane schedule and edge waste
- Core, interleaf and surface cleanliness
- Burr, camber and feed acceptance
Questions About This Cutting Application
Is foil slitting the same as cutting sheets?
No. Longitudinal slitting makes continuous narrower coils.
Does tantalum purity set the knife clearance?
No. Gauge, condition and machine geometry need a trial.
Why inspect a wound roll?
Telescoping and trapped slivers can emerge only after rewinding.
Does a clean coil qualify a capacitor part?
No. The subsequent forming and component tests are separate.
Public references and scope
These public sources provide material, cutting-method or safety context for this guide. Supplier pages describe their own materials or equipment; they do not establish a MEIRENTE blade specification or performance claim. Confirm the actual grade, machine setup and required cut with a drawing or sample.
Related product and service information
- Tantalum Metal Foil Strip Edge-Trimming Blades - tantalum metal foil · strip edge trimming
- Amorphous Metal Ribbon Precision Coil Slitting Blades - amorphous metal ribbon · precision coil slitting
- Nanocrystalline-Alloy Precursor Ribbon Precision Coil Slitting Blades - nanocrystalline-alloy amorphous precursor ribbon · precision coil slitting
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.