
Blade Application Guides / Application Guide / Specialty metal converting
Beryllium-Copper Foil Strip Edge-Trimming Blades
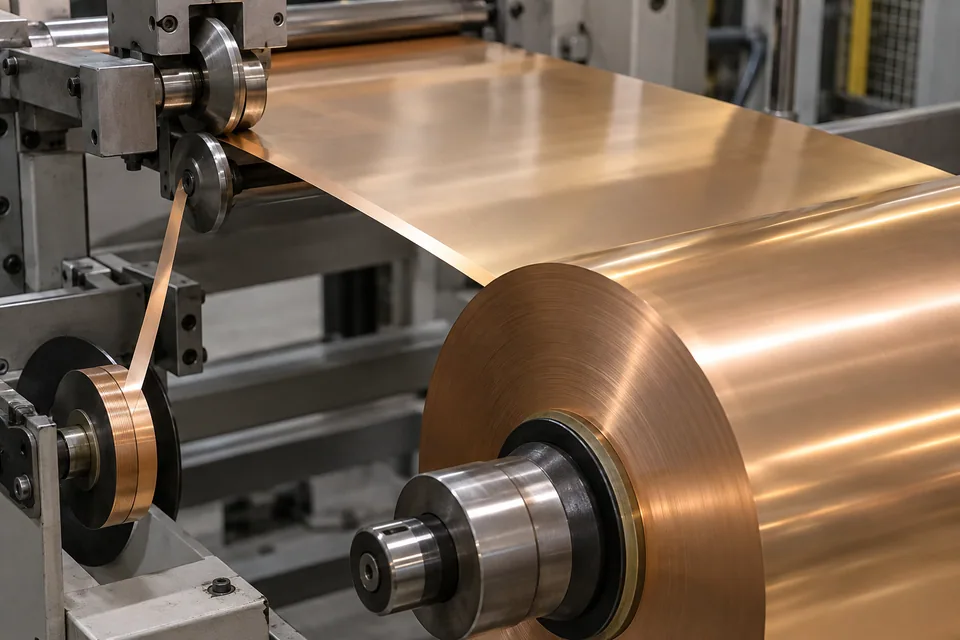
Materion describes copper-beryllium strip for precision stamped contacts and springs, and NGK Berylco identifies slitting as a continuous coil operation. Advent lists copper-beryllium foil in coil form. This makes outside-edge trimming a plausible separate finishing pass on an actual foil-grade strip, subject to its alloy, temper and thickness. Here a narrow longitudinal scrap ribbon is removed from one or both edges; the principal strip remains. This is not blanking connector shapes. The delivered edge must meet the buyer’s width, burr and later feed requirements, and the converter must follow the alloy supplier’s handling guidance.
Updated
Where This Cutting Application Appears
Define the authorized trim
Obtain alloy grade, temper, foil thickness and starting width. Locate edge cracks, handling nicks or a surplus margin that the drawing permits removing. Calculate the minimum remaining width for downstream stamping, including pilot and carrier zones. If a defect reaches into the useful band, a visually clean trim is not a valid disposition.
Support the thin strip
Guide the coil with low, repeatable side loading and support the narrow waste ribbon near its exit. Copper-beryllium in different tempers springs back differently, so compare edge curl after release rather than only under line tension. Select knife geometry and clearance with coupons from the delivered lot. Prevent the scrap from wrapping the cutter or marking the retained foil.
Inspect both edge faces
Measure retained width and straightness along the roll. Examine the trimmed side for burr, rollover, microcracks, pulled metal and a waviness that could affect progressive-die feed. Inspect the untrimmed side too, since guiding can damage it. Track burr direction so the stamping team knows which face enters its tooling.
Maintain a controlled conversion record
Identify original coil, alloy, temper, removed side and tool setup. Collect metallic scrap under the facility’s material-handling controls and do not add abrasive cleanup that could create fine airborne material. NGK’s beryllium guidance emphasizes appropriate control of particle-generating work; local safety procedures remain authoritative.
Trial the downstream feed
Run a short retained strip through the actual stamping feeder without making final parts. Check tracking, edge contact and whether a curled margin snags guides. Then inspect the first accepted stamped piece for edge-origin damage. A trim accepted by width alone can still be rejected when its edge makes the later die unstable. Compare retained width at the beginning and end of the coil, because a lateral wander can consume the stamping carrier margin before an operator notices a visible edge defect. Keep the pre-trim sample with the inspection record.
Define the Required Cut Result
- Remove only approved outside copper-beryllium foil waste.
- Keep the required stampable width and temper identity.
- Limit burr, curl and edge cracking.
- Control scrap and preserve coil traceability.
Problems to Diagnose Before Changing the Knife
Trimmed edge curls outward
- Review side loading and knife geometry.
- Measure after relaxation.
- Test feeder tracking.
Waste ribbon tears into retained foil
- Improve support and waste takeoff.
- Inspect defect depth before cutting.
- Stop if cracks propagate inward.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Supported longitudinal edge shear | For a foil-grade BeCu coil after representative trials. | Confirm width, burr direction and scrap stability. |
| Paired circular trim knives | Where the installed slitter can support thin stock. | Check both faces and coil build after rewinding. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Copper-beryllium alloy, temper and thickness
- Starting and minimum retained width
- Damaged side and permitted waste
- Burr/curl acceptance and stamp feed path
- Supplier handling instructions for scrap
Questions About This Cutting Application
Is edge trimming the same as blanking?
No. Trimming removes a narrow outer strip; blanking later separates shaped parts.
Can a damaged edge always be recovered?
Only if the remaining band meets the approved stamping width.
Why record temper?
Temper affects springback, burr and later forming behavior.
Does a good edge prove connector performance?
No. Final stamping and component testing remain separate.
Public references and scope
These public sources provide material, cutting-method or safety context for this guide. Supplier pages describe their own materials or equipment; they do not establish a MEIRENTE blade specification or performance claim. Confirm the actual grade, machine setup and required cut with a drawing or sample.
Related product and service information
- Laminated Nanocrystalline Magnetic Sheet Precision Die-Cutting Blades - laminated nanocrystalline magnetic sheet · precision die cutting
- Amorphous Metal Ribbon Strip Edge-Trimming Blades - amorphous metal ribbon · strip edge trimming
- Nanocrystalline-Alloy Precursor Ribbon Strip Edge-Trimming Blades - nanocrystalline-alloy amorphous precursor ribbon · strip edge trimming
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.