
Blade Application Guides / Application Guide / Specialty metal converting
Amorphous Metal Ribbon Precision Blanking Blades
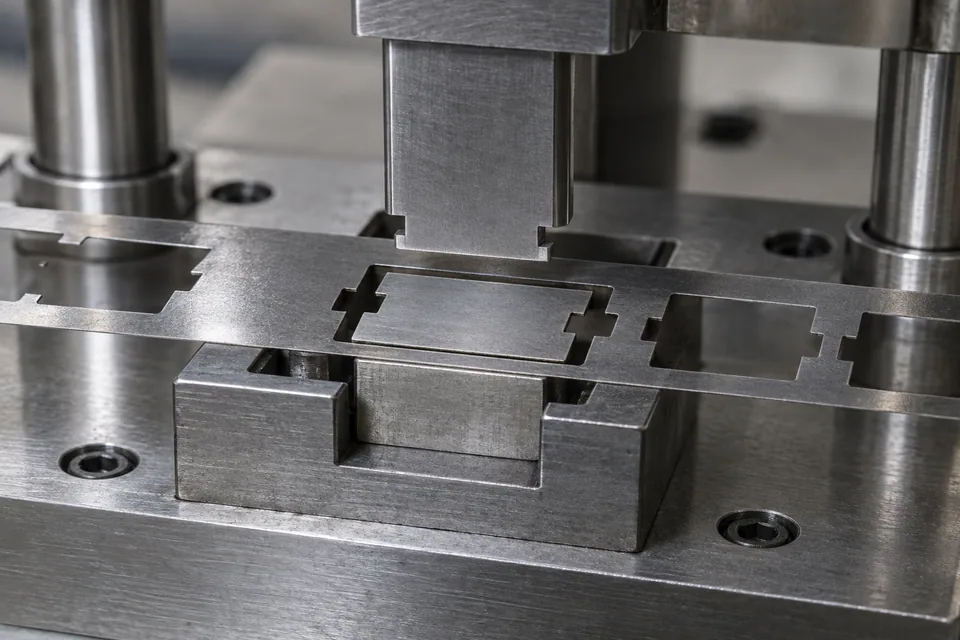
Metglas says its amorphous ribbon can be punched and stamped, while a Metglas patent describes a specific punch-and-die method for ferromagnetic amorphous strip laminations. A motor-development paper hosted by Metglas also warns that very thin amorphous ribbon is difficult to stamp or press. Those sources establish a possible route and its difficulty, not a general-purpose production setting. This guide covers a buyer-approved contour blank from loose, as-cast magnetic ribbon before stack assembly. Blanking is justified by a released outline, holes or locating features; a simple rectangular length may instead be sheared. Trial support, tool wear and scrap removal matter on thin, hard stock. The core maker must qualify the cut alloy and construction through its own magnetic tests.
Updated
Where This Cutting Application Appears
Separate magnetic part geometry from scrap web
Supply the released outline and any holes, bridges, grain or ribbon direction. Identify whether the blank forms a transformer lamination, motor segment or experimental magnetic part. The die should support useful islands while allowing skeletal scrap to leave without dragging across a finished face.
Trial the die on the specified alloy state
Record the specific alloy, as-cast state and coating or support arrangement. Trial a small batch before continuous feeding, inspecting die entry, fracture zone, slug release and edge microcracks. The Metglas patent uses a particular punch-and-die method; its settings cannot be transferred to another magnetic ribbon without testing.
Assess stack handling as well as shape
Measure critical contour features on individual blanks and inspect both faces for burrs, chips and die scratches. Stack a trial group in the intended orientation to reveal snagging, bowed parts or particle transfer. Keep part and skeleton scrap paths separate.
Tie tool wear to finished results
Retain first, middle and last cut specimens from the trial to detect changes in edge quality. Have the component maker evaluate its stack, bond or anneal sequence and test magnetic loss. Visual geometry cannot certify the completed device.
Define the Required Cut Result
- Create approved discrete contours from traceable ribbon.
- Avoid broken bridges, burrs and edge cracks.
- Keep fine scrap out of lamination stacks.
- Link die wear observations with downstream yield.
Problems to Diagnose Before Changing the Knife
Small features tear or break off
- Review punch support, part ejection and feed registration.
- Compare alloy state and tool sharpness.
One face carries a raised burr
- Inspect die clearance and wear at that contour.
- Compare cut direction and strip flatness.
Stacks develop unexplained gaps
- Look for bowed blanks, chips or snagged edge features.
- Measure each part before blaming the assembly fixture.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Matched punch and die set | For a released outline or hole pattern on a validated amorphous alloy. | Confirm feature geometry, both-face edge condition and stable scrap evacuation. |
| Simpler transverse shear | If the required part is only a straight rectangular lamination. | Compare handling yield and joint fit without assuming a die is required. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Exact amorphous alloy and delivered heat state
- Blank outline, holes, registration and direction drawing
- Ribbon width, thickness and flatness
- Part-support and feed-pilot plan
- Allowed edge crack, burr and scrap limits
- Die clearance and wear-check method
- Stack orientation and handling route
- Finished component magnetic test owner
Questions About This Cutting Application
Does a patent prove that any magnetic ribbon can be blanked?
No. It documents one method on ferromagnetic amorphous strip; the requested alloy, thickness and support need their own trial.
Why blank rather than shear?
Blanking is for a specified outline or holes; simple straight lengths may be sheared.
Why inspect the skeleton scrap?
Torn bridges and retained slugs can scratch useful blanks or jam a progressive die.
Can a dimensional pass prove magnetic performance?
No. Core or motor testing follows the approved build sequence.
What begins a useful quote?
Send the contour drawing, alloy state, coil sample and defect acceptance examples.
Public references and scope
These public sources provide material, cutting-method or safety context for this guide. Supplier pages describe their own materials or equipment; they do not establish a MEIRENTE blade specification or performance claim. Confirm the actual grade, machine setup and required cut with a drawing or sample.
Related product and service information
- Amorphous Metal Ribbon Precision Coil Slitting Blades - amorphous metal ribbon · precision coil slitting
- Beryllium-Copper Foil Precision Blanking Blades - beryllium-copper foil · precision blanking
- Tantalum Metal Foil Precision Blanking Blades - tantalum metal foil · precision blanking
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.