
Blade Application Guides / Application Guide / Electronic metal converting
Aluminum Battery-Tab Stock Strip Edge-Trimming Blades
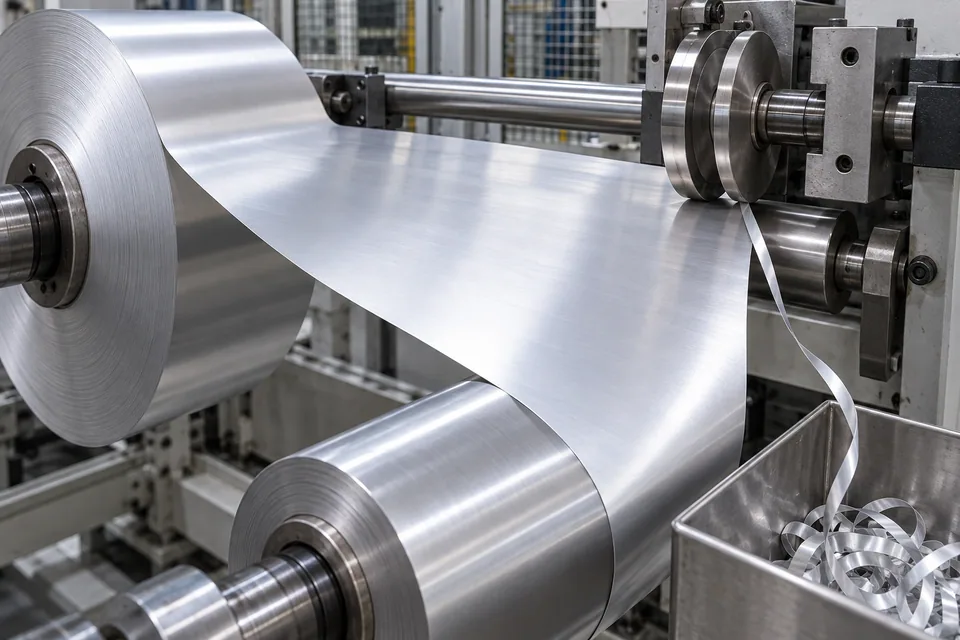
Iwatani confirms slitting of aluminum cathode-lead foil. A separate edge-trim pass is justified only where the incoming roll has a measured damaged margin or where the lead-stock drawing requires a narrower retained width. The operation removes one continuous outer scrap strip; it does not split the reel into multiple tab-width lanes. Because thin aluminum can fold or shed particles at a poorly supported cut, the retained edge must be compared with the original and the scrap path checked. The buyer must also confirm that the final width still suits the later tab cut and weld geometry. This is a coil-converting trial, not proof of battery function.
Updated
Where This Cutting Application Appears
Locate the actual bad margin
Mark the affected side, face and defect positions on a source-coil map. Measure folds, nicks or width loss against the minimum usable lead width. If defects extend across the planned cut line, hold the lot for disposition rather than claiming a narrow trim repairs it.
Keep the waste strand away from the joining face
Set one upper/lower shear pair on the specified outside edge. Guide from the sound side and lead the thin waste into its own takeoff. Observe whether it runs continuously or breaks into fragments that can enter the retained reel.
Compare new and original edges
Save paired before-and-after specimens from the same coil positions. Examine burr lip, cracks, aluminum dust and surface scratches on both faces. Measure retained width after rewind at several reel locations, including where incoming width was smallest.
Check fit in the tab route
Provide a trimmed sample to the buyer’s tab cutter or weld fixture. A slightly narrower reel can change carrier or clamp margin even when its edge looks better. Final joining and cell tests remain separate from trim approval.
Define the Required Cut Result
- Remove only the specified unusable side margin.
- Maintain the minimum useful aluminum lead width.
- Prevent new folded lips, debris and face scratches.
- Record traceable before-and-after edge evidence.
Problems to Diagnose Before Changing the Knife
Narrow trim repeatedly tears
- Review waste width and takeoff tension.
- Inspect incoming edge nicks.
A fresh lip appears on the kept edge
- Check knife support and engagement.
- Compare two faces and the original edge.
Retained reel falls below width
- Review source-width variation and guide reference.
- Measure beyond the setup position.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| One paired rotary shear station | For a mapped bad edge wholly outside the retained lead width. | Check retained-edge burr, scrap continuity and width. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Aluminum lead-stock certificate
- Identification of defective original edge
- Coil-position defect map
- Minimum retained tab-stock width
- Allowed burr, fold and particles
- Shear guide and scrap-takeoff setup
- Before-and-after specimen labels
- Later tab cutting and weld acceptance
Questions About This Cutting Application
Does every aluminum tab-stock roll need trimming?
No. Only a documented edge or width problem justifies the extra operation.
Is edge trimming the same as tab blanking?
No. Trimming removes one longitudinal margin; blanking makes discrete profiles.
Can trimming recover a crack inside the useful width?
No. That portion needs buyer-approved disposition.
Why preserve the waste path?
Broken aluminum scrap can contaminate or mark the retained lead foil.
What should the buyer send?
Provide a defect map, minimum retained width and edge acceptance examples.
Public references and scope
These public sources provide material, cutting-method or safety context for this guide. Supplier pages describe their own materials or equipment; they do not establish a MEIRENTE blade specification or performance claim. Confirm the actual grade, machine setup and required cut with a drawing or sample.
Related product and service information
- Nickel-Clad Copper Strip Cut-to-Length Blades - nickel-clad copper strip · cut to length
- Rolled-Annealed Copper Foil Strip Edge-Trimming Blades - rolled-annealed copper foil · strip edge trimming
- Ultra-Thin Stainless-Steel Foil Strip Edge-Trimming Blades - ultra-thin stainless-steel foil · strip edge trimming
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.