
Blade Application Guides / Application Guide / Specialty metal converting
Inconel Alloy Foil Cut-to-Length Blades
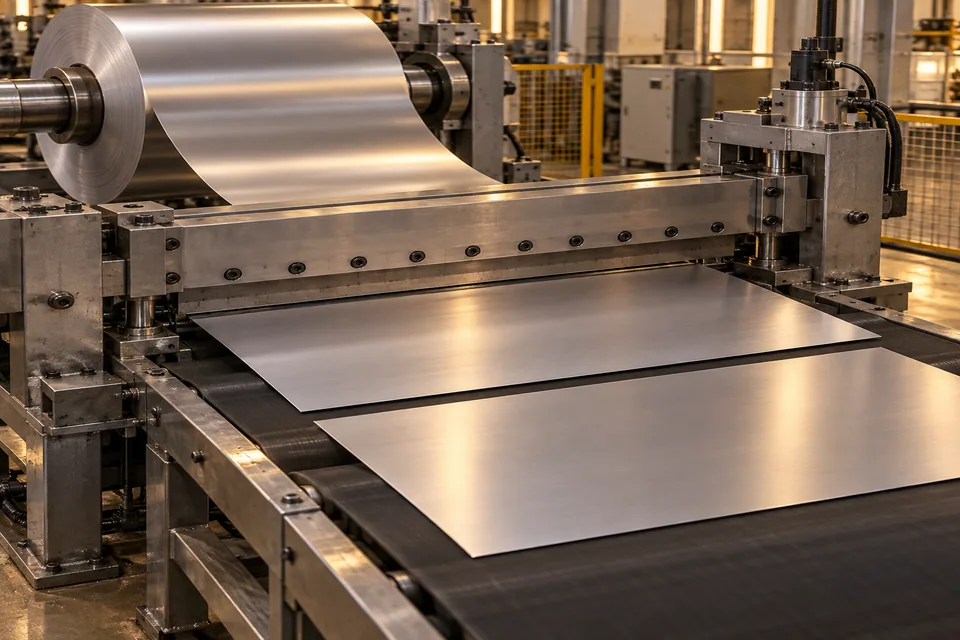
Inconel is an alloy family, not one foil grade or thickness. Ulbrich lists Inconel 600, 625, 718 and X750 among nickel alloys it supplies in foil gauges; Special Metals publishes grade-specific technical data. This guide concerns a buyer-specified thin Inconel foil coil converted into finite flat lengths. A cross-machine shear cut produces rectangular blanks; it is not longitudinal slitting and does not make a contoured component. The selected alloy, temper, gauge and surface condition govern tool fit and handling. A thin foil may wrinkle or curl when the web is unsupported even if the blade is sharp. Measure length and inspect both edges after the sheet leaves the line, with the buyer’s end-use tolerance and cleanliness method.
Updated
Where This Cutting Application Appears
Identify the exact incoming alloy
Record alloy designation, foil gauge, temper, width, surface finish and coil orientation from the certificate and buyer drawing. Do not infer that all Inconel grades respond alike. Mark which surface may contact feed rolls and which side of the finished blank is functional.
Meter and support the thin strip
Set feed length from the required blank and any head/tail crop allowance. Check guides, anti-wrinkle support and tension before the transverse shear. A skewed web can yield a trapezoid even when its centerline length is correct.
Inspect the transverse shear edge
Examine both ends for burr, roll-over, tearing, dragged metal and local curl. Compare leading and trailing cut ends; a worn or poorly supported blade can affect one side differently. Keep cut debris separate from accepted sheets and record tool condition when edge quality changes.
Assess flatness after collection
Measure blanks on the specified support after stacking or transfer, not while clamped at the cutter. Check scuffs, creases and coil set; label the grain/rolling direction if downstream forming or joining needs it. Any corrosion, heat or fatigue performance claim belongs to the owner of the final component.
Define the Required Cut Result
- Produce the specified finite foil lengths and square transverse ends.
- Limit burr, tearing, curl and surface contact marks.
- Keep alloy/lot and rolling direction traceable.
- Deliver flat blanks suitable for buyer downstream forming or joining trials.
Problems to Diagnose Before Changing the Knife
Blank length varies across its width
- Check web squareness and lateral guides.
- Inspect feed-roll slip and cut timing.
- Measure both side edges, not just centerline.
Trailing edge curls upward
- Review blade clearance and lower support.
- Compare incoming coil set.
- Inspect whether stacking adds bend after cut.
Surface scratches appear in a batch
- Map scratch location to feed rolls and collection.
- Check for trapped cut debris.
- Compare first-piece and later-piece surfaces.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Straight upper and lower transverse shear blades | For a compatible foil sheeter that meters coil into finite sheets. | Confirm actual alloy/gauge range, support and accepted burr/curl on sample material. |
| Indexed cross-cut blade with matched counteredge | When an installed narrow-web cutter uses a controlled stop-and-cut feed. | Confirm repeat length, blade engagement and no foil scuffing at the counteredge. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Exact Inconel alloy designation and material certificate
- Foil gauge, temper, width and coil inside/outside orientation
- Finished blank length, squareness and flatness drawing
- Allowed burr, roll-over and surface-mark samples
- Feed, support, knife and counteredge drawings
- Rolling direction and downstream process requirement
- Collection, interleaf and handling method
- Buyer inspection condition and sampling plan
Questions About This Cutting Application
Which Inconel grade does this guide assume?
None. The buyer must identify the exact alloy, gauge and temper; supplier data show several foil grades.
How is cut to length different from coil slitting?
Cut to length crosses the web to make finite sheets; slitting runs along the web to change width.
Can a foil sheeter handle any Inconel foil?
No. Confirm machine and blade suitability by the specified grade and a material trial.
Why inspect blank flatness after stacking?
A supported sheet can hide curl or handling creases that emerge after release.
Does a clean cut prove final alloy performance?
No. The final component owner qualifies its forming, joining and service behavior.
Public references and scope
These public sources provide material, cutting-method or safety context for this guide. Supplier pages describe their own materials or equipment; they do not establish a MEIRENTE blade specification or performance claim. Confirm the actual grade, machine setup and required cut with a drawing or sample.
Related product and service information
- Inconel Alloy Foil Precision Blanking Blades - Inconel alloy foil · precision blanking
- Cobalt Metal Foil Precision Blanking Blades - cobalt metal foil · precision blanking
- Magnesium Alloy Foil Precision Blanking Blades - magnesium alloy foil · precision blanking
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.