
Blade Application Guides / Application Guide / Flexible packaging
EVOH Barrier Film Laminate Rotary Die Cutting Blades: Layer and Barrier Integrity
An EVOH barrier film laminate uses a moisture-sensitive barrier layer within a multilayer structure selected for the package. Because layer thicknesses, tie layers and outer films vary by construction, cutting trials should focus on the supplied laminate, edge integrity and package performance instead of assuming a universal material response.
Updated
Where This Cutting Application Appears
High-barrier food pouches
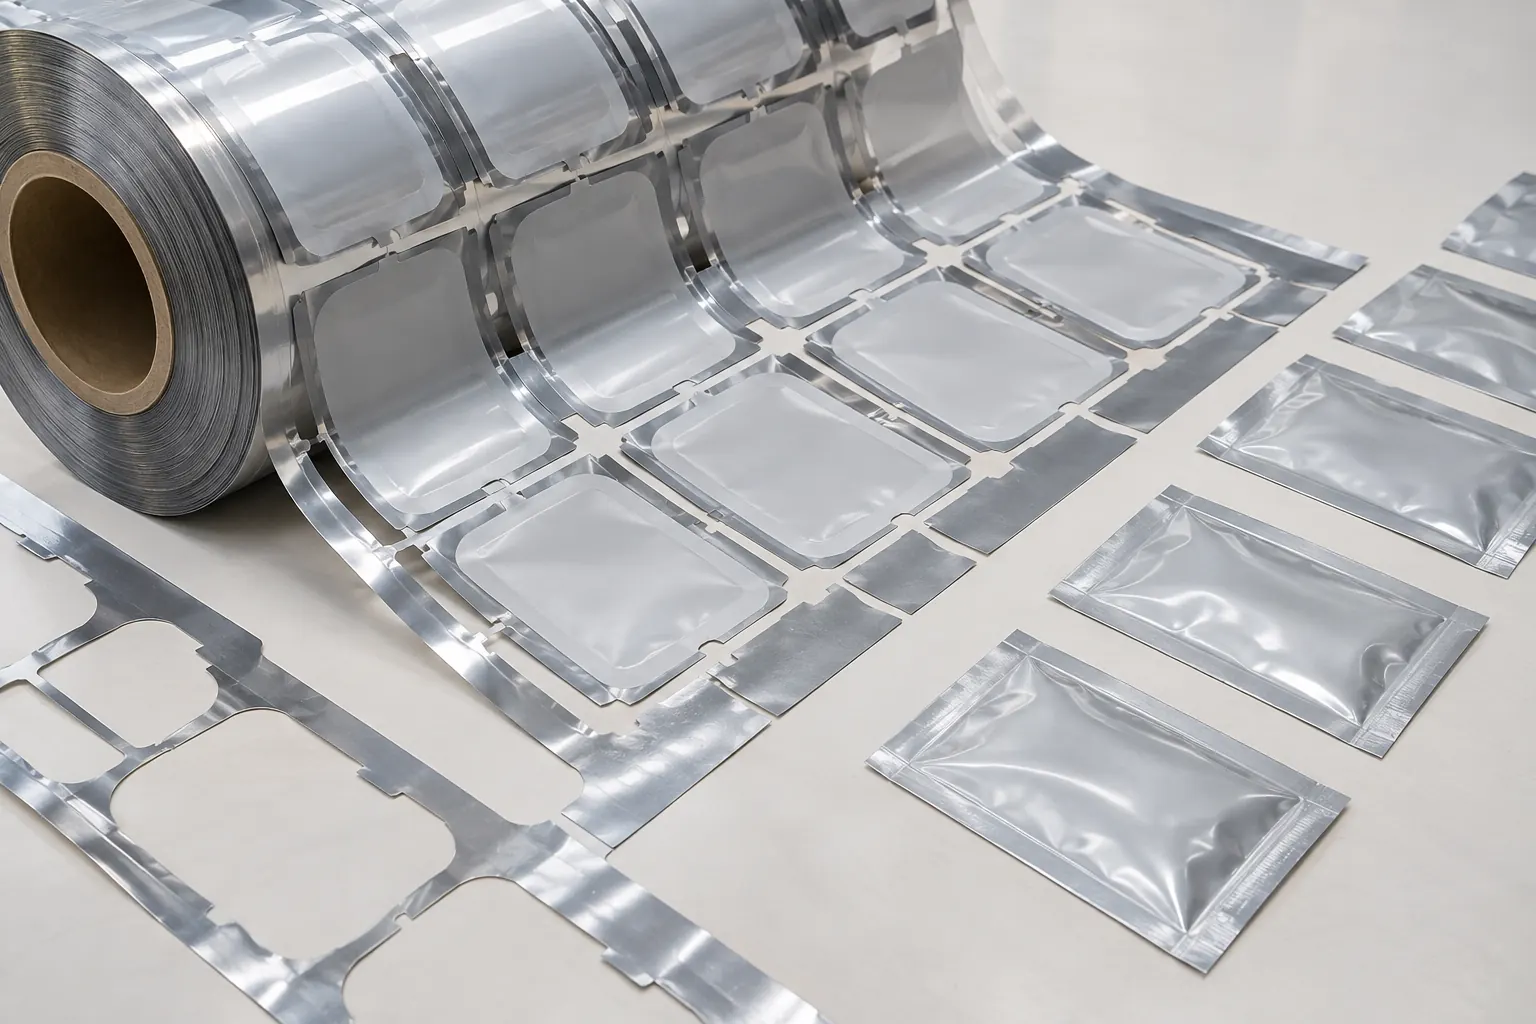
Multilayer webs are converted for oxygen-sensitive foods, where clean edges support sealing, registration and stable package geometry. During rotary die cutting, repeated profiles are produced in a moving web. Review registration, cut continuity, retained-layer condition and waste removal for this construction.
Pharmaceutical and medical overwrap
Barrier laminates are prepared for protected products, requiring traceable dimensions and no unexplained layer separation at the edge. During rotary die cutting, repeated profiles are produced in a moving web. Review registration, cut continuity, retained-layer condition and waste removal for this construction.
Barrier lidding and liner webs
EVOH-containing structures are sized for lids or liners, where width, flatness and sealing-zone cleanliness affect downstream use. During rotary die cutting, repeated profiles are produced in a moving web. Review registration, cut continuity, retained-layer condition and waste removal for this construction.
Rotary Die Cutting process boundary
Rotary die cutting repeats registered profiles with a rotating tool across a moving web; it differs from straight slitting, cross cutting and simple edge trimming.
Rotary Die Cutting setup checkpoint
Confirm repeat pitch, registration marks, anvil condition, web tension, cutting depth and the waste path for every profile and internal feature.
Rotary Die Cutting acceptance checkpoint
Inspect registration, profile dimensions, corner quality, complete separation or controlled depth, liner condition and continuous waste removal.
Define the Required Cut Result
- Create repeatable profiles with controlled penetration through the specified layers
- Hold profile position, repeat length and outline geometry within the approved tolerance
- Protect layer bonding, barrier zone and sealing surfaces
- Deliver converted material accepted for printing, pouch making, sealing and barrier verification
Problems to Diagnose Before Changing the Knife
Interlayer separation at the converted edge
Inspect layer stack, tie-layer condition, laminate cure, storage humidity, cut direction and peel behavior. Determine whether separation existed in the incoming web or initiates at the cut.
Barrier-layer exposure or edge cracking
Review the approved structure, local thickness variation, flexing after cutting and environmental conditioning. Barrier performance cannot be inferred from visual appearance alone and should follow the customer's test method.
Incomplete profiles or unintended retained-layer damage
Map uncut bridges and over-penetrated areas by lane and repeat, then review web thickness, support condition, pressure distribution and the exact layer intended to remain intact.
Registration drift or difficult matrix removal
Check print-to-cut marks, repeat pitch, web stretch, tension, waste geometry, stripping direction and whether drift develops gradually or appears at a splice.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Rotary die-cutting form | Consider when the installed equipment uses a cylindrical cutting action against a compatible support and the intended layer depth is defined. | Confirm this form only from the EVOH barrier film laminate sample, installed equipment interface, operating motion, support condition and approved drawing. |
| Replaceable rotary segment or insert form | Consider only where the existing station is engineered for replaceable cutting elements and the approved drawing defines mounting and runout requirements. | Confirm this form only from the EVOH barrier film laminate sample, installed equipment interface, operating motion, support condition and approved drawing. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Complete laminate structure and nominal thickness by layer
- EVOH grade location, tie layers and supplier handling limits
- Lamination cure status, storage humidity and roll age
- Barrier, peel and sealing acceptance methods after conversion
- Finished profile drawing, corner radii, repeat pitch and tolerances
- Layers to cut, layers to retain and allowable witness condition
- Registration-mark layout, web speed, tension and waste-stripping path
- Existing rotary-tool interface, support construction and approved sample
Questions About This Cutting Application
Does EVOH content alone determine cutting behavior during rotary die cutting?
No. Outer films, tie layers, total gauge, orientation, lamination method and conditioning can dominate the edge response. Review the complete supplied structure and representative samples.
How should barrier integrity be checked after cutting during rotary die cutting?
Use the package owner's specified barrier or package test on conditioned samples. Visual edge inspection is useful for screening but does not by itself confirm oxygen-barrier performance.
How is the intended rotary die-cutting depth specified during rotary die cutting?
Define which layers must separate and which must remain functional, then approve samples using that construction. A generic depth value is not transferable between laminates.
Why can a profile cut at one lane but bridge at another during rotary die cutting?
Cross-web gauge variation, support condition, pressure distribution, runout and web tension can change effective penetration. Map defects by lane before adjusting the setup.
What is required before quoting a rotary cutting form during rotary die cutting?
Provide the profile drawing, repeat, web construction, retained layer, machine interface, support method and representative samples. Final dimensions should follow an approved tooling drawing.
Related product and service information
- EVOH Barrier Film Laminate Cross Cutting Blades: Layer and Barrier Integrity - EVOH barrier film laminate · transverse cross cutting
- Nylon Retort Pouch Film Rotary Die Cutting Blades: Tough-Layer Edge Control - nylon retort pouch film · rotary die cutting
- Metallized PET Packaging Film Rotary Die Cutting - metallized PET packaging film · rotary die cutting
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.