
Blade Application Guides / Application Guide / Specialty metal converting
Magnesium Alloy Foil Coil Slitting Blades
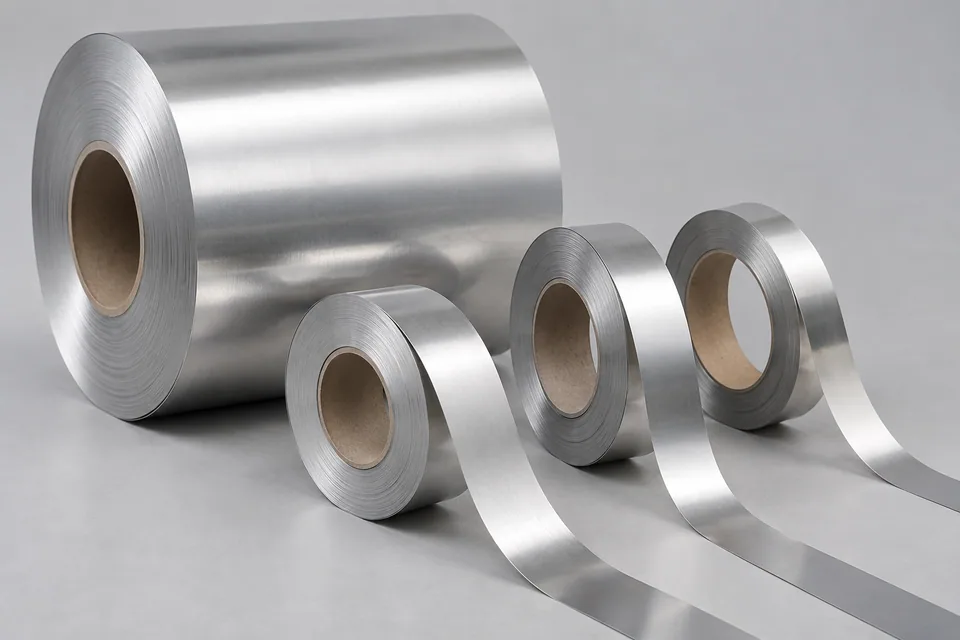
Coil slitting divides a continuous master coil into narrower strips along the feed direction. For magnesium alloy foil, the first decision is whether the proposed stock and line are suitable for the intended cut: the alloy, temper, thickness range, surface condition and acceptable finished edge must be known. A knife drawing alone cannot establish a workable clearance or safe scrap-handling method. Use a trial with the actual foil and inspect both the wound strips and their loose edges before approving a tooling specification.
Updated
Where This Cutting Application Appears
What the cut must produce
A paired rotary slitter makes parallel longitudinal cuts while the line carries the foil forward. The accepted product is a set of wound narrow coils, not an enclosed blank or a transverse sheet. Specify target widths and permissible variation for each strip position, then inspect the first, middle and last material from a trial coil.
Knife and line setup
Review the mating knife pair, arbor and spacer drawings together. Side clearance, overlap, blade condition, arbor runout and support at the cut zone can each change the edge. Record the actual setup used for an accepted sample; do not copy a clearance from another alloy or thickness without a trial.
Edge and surface acceptance
Measure strip width and inspect the slit edge for burrs, tears or distortion at an agreed sampling frequency. Check both foil faces for marks after guiding, separation and rewinding. A clean edge at the knife can still be damaged by a separator, tension change or winding contact downstream.
Trim and fines handling
Agree how narrow trim is collected and whether the process produces fine particles. Metal fines require a site-specific hazard review and suitable housekeeping and collection controls. The cutting trial should include the waste path, not only the finished strips.
Define the Required Cut Result
- Hold each finished strip within the buyer's specified width range.
- Meet the agreed burr and edge-shape limits on both slit sides.
- Keep accepted foil surfaces free of handling marks through rewinding.
- Separate and collect trim without disturbing the finished strip.
Problems to Diagnose Before Changing the Knife
Burr or ragged edges vary across the coil width
- Map the defect to knife position and inspect paired knife condition.
- Measure actual side clearance, overlap and arbor runout at that position.
- Compare foil thickness and temper across the sampled lot.
Strip width drifts during a run
- Check spacer stack, arbor seating and lateral movement.
- Compare width at the cut with width after rewinding.
- Record any tension or separator change before the drift appeared.
The slit strip wrinkles or carries face marks
- Identify the first contact point where the mark appears.
- Inspect support, guiding, separator contact and winding tension.
- Compare the trial against an untouched control sample from the same coil.
Narrow trim fails to leave the cut zone cleanly
- Check trim width, takeoff path and collection method.
- Inspect for snagging, tearing or fine-particle accumulation.
- Review the site's material-specific fire and dust controls before continuing the trial.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Matched circular slitter knife pair | For continuous longitudinal separation into multiple narrow coils on a compatible rotary slitting line. | Confirm dimensions, mounting, edge geometry and trial setup from the line drawing and actual foil sample. |
| Edge-trim knife pair | When the operation removes an outside edge before or during width conversion. | Confirm trim width, scrap takeoff and whether the resulting finished edge meets the same acceptance criteria. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Actual alloy designation, temper and foil thickness range
- Master-coil width, inner diameter, outer diameter and winding direction
- Finished strip widths, quantity and permitted width variation
- Accepted and rejected edge and surface samples, including burr limits
- Slitter knife, arbor and spacer drawings with current setup records
- Line speed, feed support, strip tension and separator arrangement
- Trim width, waste takeoff and site-specific fines-control requirements
- Trial quantity and inspection points along and across the coil
Questions About This Cutting Application
Can a knife be selected from foil thickness alone?
No. Alloy and temper, machine geometry, finished widths and the accepted edge and surface condition also determine the trial setup. Send a current line drawing and foil samples with the thickness range.
What is the difference between coil slitting and blanking?
Slitting makes continuous longitudinal strips that can be rewound as narrow coils. Blanking cuts separate shaped pieces from the stock and has different hold-down, ejection and dimensional checks.
Where should burr and width be checked?
Check both slit edges and each strip position against the agreed inspection plan. Include material from several points along the trial run and inspect the wound coil for damage that appears after the cut.
Does this guide specify a universal clearance for magnesium foil?
No. Clearance and overlap must be established against the actual alloy, foil thickness, line condition and accepted sample. A universal value would hide those differences.
What should be discussed before trialing the waste path?
Confirm the amount and form of trim or fines, their collection route and the site's material-specific fire and dust controls. Magnesium-containing fines can require additional precautions.
Public references and scope
These public sources provide material, cutting-method or safety context for this guide. Supplier pages describe their own materials or equipment; they do not establish a MEIRENTE blade specification or performance claim. Confirm the actual grade, machine setup and required cut with a drawing or sample.
Related product and service information
- Zinc Metal Foil Coil Slitting Blades - zinc metal foil · coil slitting
- Inconel Alloy Foil Coil Slitting Blades - Inconel alloy foil · coil slitting
- Cobalt Metal Foil Coil Slitting Blades - cobalt metal foil · coil slitting
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.