
Blade Application Guides / Application Guide / Advanced solar manufacturing
Solar Interconnect Copper Foil Razor Slitting Blades
Solar Interconnect Copper Foil is a thin barrier, encapsulation, sealing or conductive layer whose optical and interface performance must survive converting. During razor slitting, the objective is to divide thin moving web stock with a low-force razor entry while preventing edge cracks, barrier damage, adhesive transfer, curl or metallic burrs. Blade selection should follow samples, machine drawings and measurable acceptance criteria rather than the material name alone.
Updated
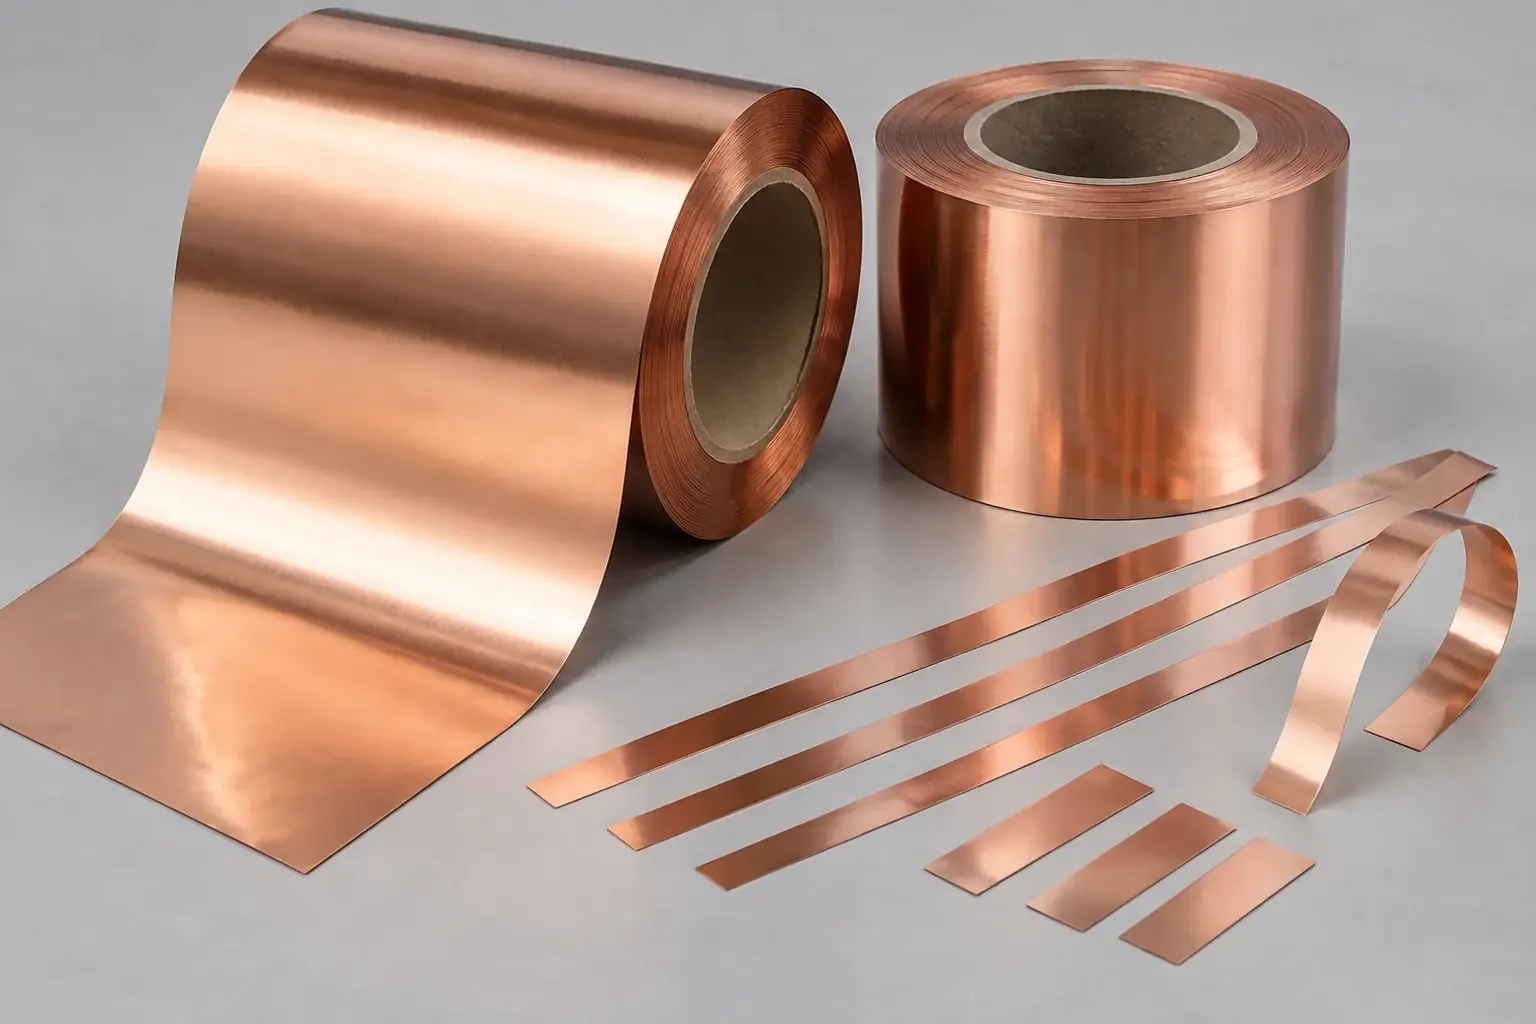
Where This Cutting Application Appears
Advanced solar manufacturing production
Solar Interconnect Copper Foil is processed by razor slitting to support solar-cell interconnection, environmental sealing and long-term module protection. The finished result must remain compatible with downstream handling, inspection and assembly.
Cut-quality control
Production teams compare accepted and rejected samples for edge integrity, width, coating continuity, barrier condition, curl and surface cleanliness, then relate the result to entry angle, blade exposure, web support, tension, runout and debris extraction.
Stable material and waste handling
Low-tension web support, clean contact surfaces and controlled narrow-waste removal help the product and waste leave the cut zone consistently without creating a second defect after separation.
Razor Slitting process boundary
Razor slitting uses a stationary thin edge through a supported or free web; it is not a paired circular shear cut.
Production setup checkpoint
Record the starting setup for entry angle, blade exposure, web support, tension, runout and debris extraction, then change one controlled variable at a time and retain samples from each trial condition.
Cut-quality acceptance checkpoint
Approve the result against measured edge integrity, width, coating continuity, barrier condition, curl and surface cleanliness after the sample has reached the same handling or conditioning state used by the next production step.
Define the Required Cut Result
- Achieve stable narrow widths with low drag and clean web edges for solar interconnect copper foil
- Prevent edge cracks, barrier damage, adhesive transfer, curl or metallic burrs
- Maintain the required geometry for solar-cell interconnection, environmental sealing and long-term module protection
- Deliver a cut condition accepted by the next advanced solar manufacturing operation
Problems to Diagnose Before Changing the Knife
The processed material shows edge cracks, barrier damage, adhesive transfer, curl or metallic burrs
- Compare blade condition and clearance.
- Check entry angle, blade exposure, web support, tension, runout and debris extraction.
- Separate material-lot effects from machine effects.
Finished dimensions drift during a production run
- Check feed registration and tension or hold-down.
- Measure runout, temperature and support condition.
- Record when dimensions are measured after cutting.
The workpiece shifts, curls or loses functional surface quality
- Review low-tension web support, clean contact surfaces and controlled narrow-waste removal.
- Confirm material direction and contact-face cleanliness.
- Identify the first point where deformation appears.
Product and waste do not separate consistently
- Check cut completeness and waste width.
- Review exit angle, static and extraction.
- Inspect downstream transfer and collection tension.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Industrial razor slitting blade | Considered when razor slitting requires stable narrow widths with low drag and clean web edges under stable support and guidance. | Confirm only after reviewing a real solar interconnect copper foil sample, the equipment interface, mounting drawing, operating direction and an accepted cut reference. |
| Three-hole slitter razor | Considered when the equipment interface and material response require an alternative geometry or cutting motion. | Confirm only after reviewing a real solar interconnect copper foil sample, the equipment interface, mounting drawing, operating direction and an accepted cut reference. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Solar Interconnect Copper Foil composition, grade, thickness and allowable lot variation
- Layer, coating, temper, adhesive or surface-function details relevant to razor slitting
- Input width and target dimensions, tolerances and acceptance drawing
- Line speed, feed mode, tension or hold-down, temperature and cutting frequency
- Current blade or knife drawing, holder interface, mounting dimensions and used sample
- Material direction, support, contact faces and product or waste collection method
- Accepted and rejected samples with limits for edge integrity, width, coating continuity, barrier condition, curl and surface cleanliness
- Trial quantity, inspection method, downstream operation, packing and annual demand
Questions About This Cutting Application
Why must solar interconnect copper foil be reviewed as a complete material construction?
Its layers, surface condition and mechanical response can react differently to pressure, friction, heat and bending, so nominal thickness alone does not predict razor slitting performance.
Can the blade be selected from the material name alone?
No. Confirm entry angle, blade exposure, web support, tension, runout and debris extraction, the holder interface, production speed, support and accepted samples before fixing blade material or edge geometry.
What commonly causes defects during razor slitting?
Material variation, unstable support, alignment error, contamination, inappropriate clearance and blade wear can interact to create edge cracks, barrier damage, adhesive transfer, curl or metallic burrs.
When should the finished result be measured?
Record both immediate and conditioned results when recovery, residual stress, temperature, moisture or adhesive flow can change the workpiece after cutting.
What should be recorded during a production trial?
Record the solar interconnect copper foil lot, setup, speed, support, blade condition, dimensions, edge observations, waste behavior and downstream acceptance.
Related product and service information
- Solar Interconnect Copper Foil Shear Slitting Blades - solar interconnect copper foil · shear slitting
- Perovskite Solar Barrier Film Razor Slitting Blades - perovskite solar barrier film · razor slitting
- Solar Ribbon Cover Film Razor Slitting Blades - solar ribbon cover film · razor slitting
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.