
Blade Application Guides / Application Guide / Rubber processing
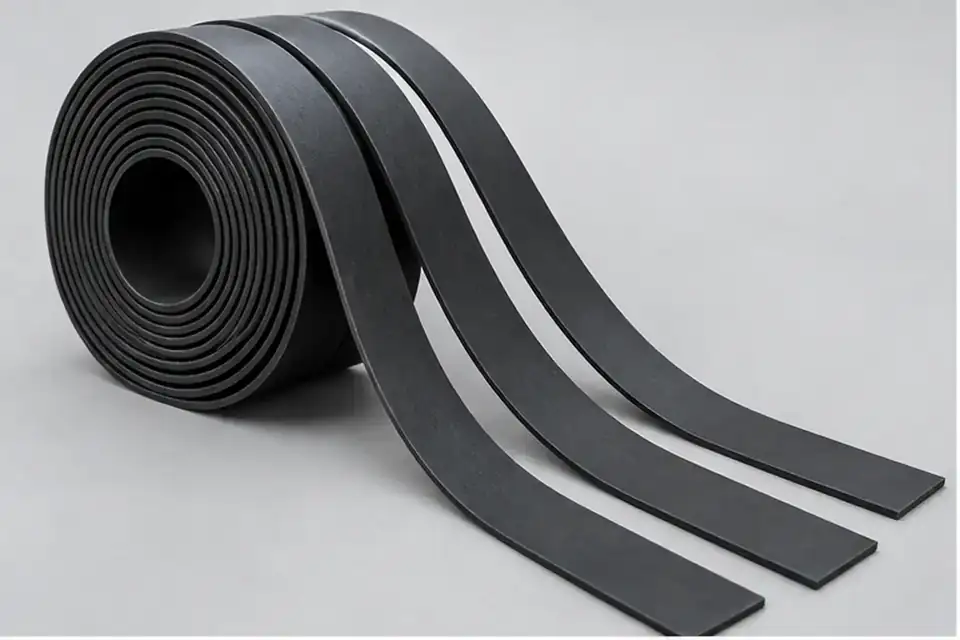
EPDM Roofing Rubber Sheet Slitting Blades
EPDM Roofing Rubber has an elastic sheet or sealing compound that can compress, recover, drag or smear during conversion. For sheet slitting, review elastomer type, hardness and thickness, reinforcement, surface finish and release treatment, support, operating speed and the actual equipment interface together. Compare accepted and rejected samples for slit width drifts across the web and elastic recovery moves the finished dimension before confirming a knife configuration.
Updated
Where This Cutting Application Appears
Industrial Gasket Production
EPDM Roofing Rubber is converted by sheet slitting for industrial gasket production, where narrow rolls with parallel clean edges supports reliable production.
Fluid-Sealing Components
EPDM Roofing Rubber is converted by sheet slitting for fluid-sealing components, where consistent geometry and protected functional surfaces supports reliable production.
Automotive And Appliance Seals
EPDM Roofing Rubber is converted by sheet slitting for automotive and appliance seals, where repeatable handling in the next assembly step supports reliable production.
Sheet Slitting process boundary
Sheet slitting divides sheet stock along parallel longitudinal lines to create strips; it is not final rectangular sizing or a shaped profile cut.
Sheet Slitting setup checkpoint
Confirm sheet support, parallel guide references, blade-line spacing and how narrow strips leave the cutting zone without rotating or overlapping.
Sheet Slitting acceptance checkpoint
Inspect strip width at several positions, edge straightness, surface marking and whether the strips remain flat enough for the next operation.
Define the Required Cut Result
- Hold slit width and edge straightness across the master roll
- Build stable rewind rolls without telescoping or blocking
- Control the material-specific risk: elastic recovery moves the finished dimension
- Keep the converted EPDM roofing rubber suitable for industrial gasket production after sheet slitting
Problems to Diagnose Before Changing the Knife
Slit width drifts across the web
Check web guiding, shaft runout, spacer stack, side load, tension and roll hardness.
Elastic recovery moves the finished dimension
Compare elastomer type, hardness and thickness, temperature, support, speed and samples from accepted and rejected positions.
Edge drags, tears or develops a raised lip
Review reinforcement, surface finish and release treatment, web orientation, contact surfaces, tension and downstream acceptance.
EPDM roofing rubber handling becomes unstable after sheet slitting
Trace separation, transfer and collection from the cut point into industrial gasket production, and record where the first unstable condition appears.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Circular shear slitting arrangement | For supported precision width conversion with controlled overlap and side load. | Confirm only from the actual EPDM roofing rubber sample, equipment interface, operating motion, current component and approved drawing. |
| Score or crush slitting arrangement | Only where the material and compatible anvil system support controlled penetration. | Confirm only from the actual EPDM roofing rubber sample, equipment interface, operating motion, current component and approved drawing. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- elastomer type, hardness and thickness
- reinforcement, surface finish and release treatment
- master-roll width, diameter, core and required slit widths
- Sheet slitting speed, feed or tension, temperature, support and cutting frequency for EPDM roofing rubber
- Current cutting arrangement, holder or rotor drawing, mounting dimensions and a labelled used sample
- EPDM roofing rubber direction, contact faces, guiding and product or waste collection route
- Accepted and rejected EPDM roofing rubber samples with measurable edge, surface, particle and dimensional limits
- Trial quantity, inspection method, industrial gasket production requirement, packing and annual demand
Questions About This Cutting Application
Why must EPDM roofing rubber be reviewed as a complete construction?
Review elastomer type, hardness and thickness together with reinforcement, surface finish and release treatment; these properties can change the response to support, pressure, speed and temperature during sheet slitting.
Can the blade configuration be selected from the term “EPDM roofing rubber” alone?
No. Confirm the sheet slitting motion, holder interface, support, speed, dimensions and accepted samples before selecting a configuration.
What commonly causes defects during sheet slitting?
Slit width drifts across the web and elastic recovery moves the finished dimension can come from interacting material, support, alignment, speed and handling conditions, so accepted and rejected samples should be compared at the same production settings.
When should converted dimensions be measured?
Measure the EPDM roofing rubber at the agreed inspection point and again after any conditioning or downstream handling that can change the accepted dimension or edge condition.
What should a production trial record?
Record the material lot, sheet slitting setup, operating speed, support, dimensions, slit width drifts across the web and performance in industrial gasket production.
Related product and service information
- Fluoroelastomer Rubber Sheet Edge Trimming Blades - fluoroelastomer rubber sheet · edge trimming
- Silicone Rubber Sheet Slitting Blades - silicone rubber sheet · sheet slitting
- Neoprene Sponge Rubber Sheet Slitting Blades - neoprene sponge rubber · sheet slitting
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.