Blade Application Guides / Application Guide / Pharmaceutical device manufacturing
Diagnostic Reagent Pouch Laminate Rotary Die Cutting Blades
Diagnostic Reagent Pouch Laminate is a pharmaceutical packaging or delivery laminate whose barrier, adhesive and functional layers must remain intact and clean. During rotary die cutting, the objective is to produce repeat profiles at production speed while preventing barrier-layer cracking, adhesive transfer, foil burr, delamination or incomplete matrix separation. Blade selection should follow samples, equipment drawings and measurable acceptance criteria rather than the material name alone.
Reviewed by the MEIRENTE technical team · Updated September 13, 2026
Where This Cutting Application Appears
Pharmaceutical device manufacturing production
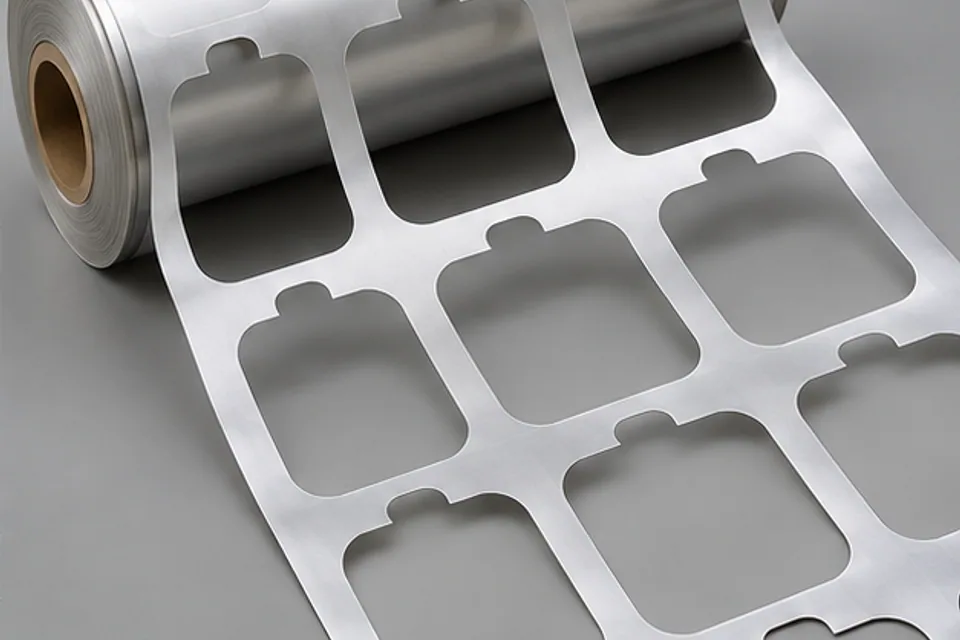
Diagnostic Reagent Pouch Laminate is processed by rotary die cutting to support transdermal delivery, unit-dose packaging, diagnostic reagents and controlled pharmaceutical dispensing. The finished geometry must remain compatible with downstream handling and assembly.
Cut-quality control
Production teams compare accepted and rejected samples for profile dimensions, edge integrity, barrier continuity, seal area, particle level and package compatibility, then relate the result to repeat pitch, anvil condition, cutting pressure, registration and matrix path.
Stable material and waste handling
clean supported conversion, controlled liner release and protected transfer into pharmaceutical packaging help the product and waste leave the cut zone consistently without creating a second defect after separation.
Rotary Die Cutting process boundary
Rotary die cutting repeats registered profiles with a rotating tool across a moving web; it differs from straight sheet cutting and may include through-cut or controlled-depth zones.
Diagnostic Reagent Pouch Laminate setup checkpoint
Record the diagnostic reagent pouch laminate lot, thickness, direction, support, repeat pitch, anvil condition, cutting pressure, registration and matrix path, operating speed and initial cut condition before changing one variable at a time.
Diagnostic Reagent Pouch Laminate acceptance checkpoint
Release the setup only after accepted diagnostic reagent pouch laminate samples meet documented limits for profile dimensions, edge integrity, barrier continuity, seal area, particle level and package compatibility and remain suitable for transdermal delivery, unit-dose packaging, diagnostic reagents and controlled pharmaceutical dispensing.
Common Ways to Describe This Cutting Problem
- diagnostic reagent pouch laminate rotary die cutting blades
- industrial diagnostic reagent pouch laminate rotary die cutting blades
- custom diagnostic reagent pouch laminate blades for rotary die cutting
- how to improve rotary die cutting of diagnostic reagent pouch laminate
- diagnostic reagent pouch laminate rotary die cutting edge defect analysis
- diagnostic reagent pouch laminate rotary die cutting dimensional control
- Pharmaceutical device manufacturing diagnostic reagent pouch laminate rotary die cutting setup
- diagnostic reagent pouch laminate blade RFQ data for rotary die cutting
Define the Required Cut Result
- Achieve registered parts and stable waste-matrix separation for diagnostic reagent pouch laminate
- Prevent barrier-layer cracking, adhesive transfer, foil burr, delamination or incomplete matrix separation
- Maintain the required geometry for transdermal delivery, unit-dose packaging, diagnostic reagents and controlled pharmaceutical dispensing
- Deliver a cut condition accepted by the next pharmaceutical device manufacturing operation
Problems to Diagnose Before Changing the Knife
The cut edge shows barrier-layer cracking, adhesive transfer, foil burr, delamination or incomplete matrix separation
Compare blade condition, repeat pitch, anvil condition, cutting pressure, registration and matrix path, material lot and accepted versus rejected samples.
Finished dimensions drift during a production run
Check feed registration, tension or hold-down, temperature, support condition, runout and when dimensions are measured.
The workpiece shifts, curls or loses functional surface quality
Review clean supported conversion, controlled liner release and protected transfer into pharmaceutical packaging, contact-face cleanliness, material direction, support and the first point where deformation appears.
Product and waste do not separate consistently
Check cut completeness, waste width, exit angle, static, extraction, collection tension and downstream transfer.
Knife Forms That May Be Considered
| Possible knife form | When it may be considered | What must be confirmed |
|---|---|---|
| Rotary die-cutting blade | Considered when rotary die cutting requires registered parts and stable waste-matrix separation under stable support and guidance. | Confirm only after reviewing a real diagnostic reagent pouch laminate sample, the equipment interface, mounting drawing, operating direction and an accepted cut reference. |
| Magnetic-cylinder flexible die | Considered when the equipment interface and material response require an alternative geometry or cutting motion. | Confirm only after reviewing a real diagnostic reagent pouch laminate sample, the equipment interface, mounting drawing, operating direction and an accepted cut reference. |
Information to Send for Technical Review
You do not need to know the exact blade name. Send the available workpiece, machine, current-knife and cut-result information so the application can be reviewed against a drawing or sample.
- Diagnostic Reagent Pouch Laminate composition, grade, thickness and allowable lot variation
- Layer, coating, porosity, temper, adhesive or surface-function details relevant to rotary die cutting
- Input width and target dimensions, tolerances and acceptance drawing
- Line speed, feed mode, tension or hold-down, temperature and cutting frequency
- Current blade or knife drawing, holder interface, mounting dimensions and used sample
- Material direction, support, contact faces and product or waste collection method
- Accepted and rejected samples with limits for profile dimensions, edge integrity, barrier continuity, seal area, particle level and package compatibility
- Trial quantity, inspection method, downstream operation, packing and annual demand
Questions About This Cutting Application
Why must diagnostic reagent pouch laminate be reviewed as a complete material construction?
Its substrate, coating, interfaces and surface condition can respond differently to pressure, friction and bending, so nominal thickness alone does not predict rotary die cutting performance.
Can the blade be selected from the material name alone?
No. Confirm repeat pitch, anvil condition, cutting pressure, registration and matrix path, the holder interface, production speed, support and accepted samples before fixing the blade geometry.
What commonly causes defects during rotary die cutting?
Material variation, unstable support, alignment error, contamination, inappropriate clearance and blade wear can interact to create barrier-layer cracking, adhesive transfer, foil burr, delamination or incomplete matrix separation.
When should the finished dimensions be measured?
Record both immediate and conditioned results when recovery, residual stress, temperature, moisture or adhesive flow can change the part after cutting.
What should be recorded during a production trial?
Record the diagnostic reagent pouch laminate lot, setup, speed, support, blade condition, dimensions, edge observations, waste behavior and downstream acceptance.
Related product and service information
- Diagnostic Reagent Pouch Laminate Sheet Cutting Blades - diagnostic reagent pouch laminate · sheet cutting
- Transdermal Drug Reservoir Film Rotary Die Cutting Blades - transdermal drug reservoir film · rotary die cutting
- Buccal Drug Delivery Film Rotary Die Cutting Blades - buccal drug delivery film · rotary die cutting
Request a Custom Cutting-Knife Review
Send the workpiece details, machine or holder information, current knife photos or sample, required quantity and examples of the present cut problem. Final dimensions, material, edge geometry and tolerances are confirmed from the approved requirements.